Contact Platform Support
 Help Center
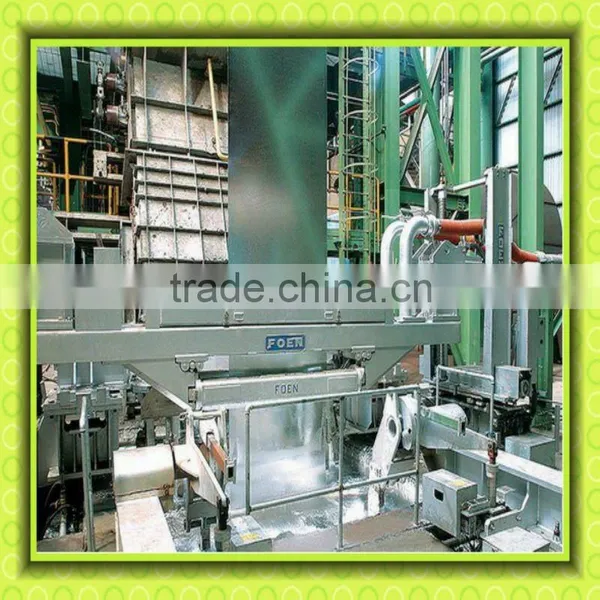
Hot Dip Galvanizing Production Line

Related Products
-
 Auto/Semi-auto Steel Strip Hot Dip Galvanizing MachineUS$ 46,000 - 1,000,000MOQ: 1 Set
-
Striped Steel Hot Dip Galvanizing MachineUS$ 46,000 - 1,000,000MOQ: 1 Set
-
High Quality Striped Steel Hot Dip Galvanizing LineUS$ 46,000 - 1,000,000MOQ: 1 Set
-
Steel Strap Hot Dip Galvanizing MachineryUS$ 46,000 - 1,000,000MOQ: 1 Set
-
Electricity Steel Strap Hot Dip Galvanizing MachineryUS$ 46,000 - 1,000,000MOQ: 1 Set
Dear Customers,
This is Ada,thanks for your interest in our products. The following is for your reference, we have our own design teams and factory ,we can design according to your requirement.Welcome your inquiry,I will reply you as soon as possible.
Hot Dip Galvanizing production line/production machinery
A.Production Line Design and manufacture conditions
1. Quality requirements of Products must according to Structure Part, Standard Part Standard rule
2. Size of Zinc Pot: 2.5*2.0*2.5(m)
3. Zinc Capacity: 87.5T
4. Galvanizing method by hanging of crane
5. Processing Temperature 430~450°C
6. Employee 8~12 Person/ Group
7. Capacity 10000~15000Tons/Year(One year as 300 Days)
8. Kettle Power Supply 720kw
9. Production Line Length Accorded with Drawing
10. Workshop Height Accorded with Drawing
11. Workshop Width Accorded with Drawing
12. Rated voltage V (As Per Customer)
13. Frequency Hz (As Per Customer)
B.Production Processing
Spare parts preplating→Degrease disposing→Rinsing→Pickling derusting→Rinsing→Dip Auxiliary agent→Spare parts drying→hot dip galvanizing→Water cooling→Passivation→Checking, Repairing and cleaning→Packing
C.Description of the process
1. Spare parts preplating.
According to different products structure,put all the Spare parts on the Hanger,Use rail car carry to Galvanizing Area for Preparation
2. Degrease disposing.
Let Crane lifting hanger to Degrease disposing Tank, Use chemical surface treating agent cleaning the spare parts. Degrease disposing Temperature 50~80 C, Use Anti-corrosion electrical heating
3. Pickling derusting.
Let spare parts lifting form Degrease disposing Tank to Acid pickling Tank, Then use CITRANOD to clean oxide and other impurity. Pickling derusting Temperature Room temperature ~40°C, Use Anti-corrosion electrical heating.
4. Deacidification Cleaning.
Let spare parts into Rinsing Area, Cleaning the Acid residue,Avoid acid residue into next steps.
5. Dip Auxiliary agent.
Let Crane put the spare parts into Assisted plating liquid. Then coated with Assisted plating liquid, in this way, Both Avoid spare parts second oxidation, And promote spare parts affinity with zinc solution, Improve Galvanized quality,Temperature 50~75°C, Use Anti-corrosion electrical heating.
6. Spare parts drying:Because Assisted plating liquid is aqueous solution, Before spare parts into Zinc Pot, Must Drying the surface of spare parts, Avoid splash Zinc or other conditions, All the pretreatment has finished.
7. Hot dip galvanizing.
Structure Part Let after-drying spare parts lifting from Drying furnace, Use Travelling Crane move into zinc solution, And according to different spare parts and galvanized process control time and temperature.
Galvanizing Temperature:430~450 C
8.Water Cooling and Passivation.
9. After Galvanizing Repair
After Spare parts cooling, check the Galvanizing Quality, If some goods not qualified, must repair and Galvanizing again, Then packed qualified goods, put into warehouse
If you need more information,please feel free to contact me.
Best wishes
Skype:adawei1019
Moibile:0086-13662169442

Send Inquiry to This Supplier

You May Also Like
-
40T Electric Tilting Machine for Heavy Parts RotationNegotiableMOQ: 1 Set
-
Efficient Copper Cable Granulator for Scrap Wire RecyclingNegotiableMOQ: 1 Set
-
PLC Controlled Food Machine 500kg/h Capacity 304 Stainless Steel IP65 Waterproof PanelUS$ 200MOQ: 1 Acre
-
Automatic/manual Fluidized Bed Dip Powder Coating Equipment Line for Refrigerator Shelves ProductionUS$ 2000 - 40000MOQ: 1 Set
-
Double Shaft Shredder Unit, Heavy‑Duty Two‑Shaft Shredding Equipment for Scrap Metal, Tyre, Plastic and Wood Waste Recycling ProjectsNegotiableMOQ: 1 Set
-
Large Gear Ring for Wind Turbine Gearbox, 17CrNiMo6, Carburizing Quenching, Up to 4000mm, Mill Test ReportUS$ 1000MOQ: 1 Combo
-
Rotary Kiln Plant Design Solution 500 TpdUS$ 2000 - 80000MOQ: 1 Set
-
Vertical Scrap Metal Baler With 5.5kW Motor & Safety Lock SystemNegotiableMOQ: 1 Set
-
Automatic Gabion Basket Wire Mesh Forming and Welding MachineNegotiableMOQ: 1 Set
-
Metal Zipper Chemical Cold Plating Machine (13 Tanks)US$ 1,000 - 10,000MOQ: 1 Set