Contact Platform Support
 Help Center
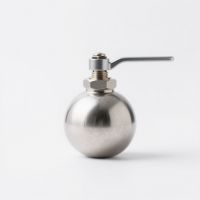
Energy-Efficient S100B Liquid Level Regulator Valve for Industrial Applications




Related Products
-
 Commercial Vehicle Height Control Valve S100C, Precision Leveling for Enhanced StabilityNegotiableMOQ: 1 Set
-
S100C Air Suspension Height Control Valve With Durable Construction, Fits Multiple ModelsNegotiableMOQ: 1 Set
-
S100C Height Control Valve for Commercial Vehicle Air Suspension Systems, Heavy Duty DesignNegotiableMOQ: 1 Set
-
OEM Replacement S100C Height Control Valve for Air Suspension, Corrosion Resistant MaterialNegotiableMOQ: 1 Set
-
S100C Height Control Valve for Bus and Truck Air Suspension, Reliable PerformanceNegotiableMOQ: 1 Set
Shanghai Sote Valve Co., Ltd., a specialized industrial valve manufacturer based in Shanghai, China, introduces the Energy-Efficient S100B Liquid Level Regulator Valve. This precision-engineered solution addresses critical level control challenges in demanding industrial environments. Our valve ensures operational reliability while significantly reducing energy costs through intelligent fluid management.
Engineered for heavy-duty applications, the S100B maintains optimal liquid levels in systems where consistency directly impacts productivity. The innovative design incorporates advanced flow dynamics to minimize pressure loss and prevent system overflow, delivering tangible operational benefits for facilities managers and process engineers.
Core Technical Specifications:
| Parameter | Specification |
|---|---|
| Body Material | 316 Stainless Steel (Standard) |
| Sealing Components | EPDM / Viton (Optional) |
| Maximum Flow Rate | 50 GPM @ 100 PSI |
| Actuation Type | Pilot-Operated Diaphragm |
| Response Time | < 3 Seconds |
Performance Advantages:
- ✓ Precision Level Control: Maintains liquid levels within ±5mm tolerance through integrated float mechanism
- ✓ Energy Conservation: Reduces pump cycling frequency by 40% compared to conventional valves
- ✓ Zero-Leakage Design: Double-sealed stem assembly prevents process fluid loss
- ✓ Corrosion Resistance: Full metallic construction suitable for aggressive media
- ✓ Maintenance Optimization: Field-serviceable components reduce downtime by 60%
The S100B's modular architecture allows for straightforward adaptation to existing infrastructure without complex retrofitting. The valve's fail-safe operation ensures automatic shutdown during abnormal conditions, protecting downstream equipment from damage. Installation flexibility is enhanced through multiple mounting orientations and optional remote monitoring ports.
Industrial Implementation Benefits:
- • Extends equipment lifespan by preventing dry-running and overflow conditions
- • Reduces water treatment costs by minimizing makeup water requirements
- • Compatible with SCADA integration for centralized process monitoring
- • Suitable for steam condensate systems, cooling towers, and chemical processing
Shanghai Sote Valve's manufacturing expertise ensures each S100B valve undergoes rigorous pressure testing and functional validation. Our Shanghai-based production facility maintains ISO-compliant quality processes, though specific certifications can be provided upon customer request. With over 15 years of industrial flow control experience, we support clients through customized engineering solutions and responsive technical service.
Implement the S100B to achieve measurable reductions in operational expenses while enhancing system reliability. Contact our engineering team today to discuss your specific application requirements and receive a detailed performance analysis. We offer comprehensive technical documentation and onsite support for seamless integration into your existing processes.
Frequently Asked Questions:
Q1: What maintenance intervals are recommended for the S100B valve?
A: Under normal operating conditions, we recommend inspection every 6 months and preventative maintenance annually. The modular design allows component replacement without full valve removal.
Q2: Can this valve handle high-temperature applications?
A: Yes, the standard configuration operates reliably up to 120°C. Special high-temperature versions (up to 180°C) are available upon request.
Q3: Is the valve compatible with aggressive chemicals?
A: Compatibility depends on concentration and temperature. We offer alternative sealing materials including PTFE and FFKM for challenging media. Consult our chemical resistance chart.
Q4: What is the lead time for custom configurations?
A: Standard models ship within 7 working days. Customized units typically require 3-4 weeks depending on specifications.
Q5: Does the valve require external power?
A: No, the S100B operates purely through hydraulic pressure and mechanical actuation, making it ideal for hazardous locations.
Q6: Can I integrate this with existing PLC systems?
A: Yes, optional position feedback sensors (4-20mA or discrete signal) are available for automation integration.
Q7: What is the warranty period?
A: We provide a standard 24-month warranty against manufacturing defects, extendable through service contracts.
Q8: Are installation kits included?
A: Basic mounting hardware is provided. Application-specific installation kits with adapters and gaskets are available separately.

Send Inquiry to This Supplier


You May Also Like
-
S100C Height Control Valve for Commercial Vehicles, Ensures Optimal Load DistributionNegotiableMOQ: 1 Set
-
Durable S100C Height Control Valve for Air Suspension Systems, High Temperature ResistanceNegotiableMOQ: 1 Set
-
Precision S200x Pressure Control Valve With High Flow Capacity and Corrosion-Resistant ConstructionNegotiableMOQ: 1 Piece
-
S200x Direct Acting Pressure Reducing Valve With NPT Threads and Adjustable Pressure SettingNegotiableMOQ: 1 Piece
-
S200x Pressure Reducing Valve for Water Supply Systems With Stainless Steel Body and Brass TrimNegotiableMOQ: 1 Piece
-
Reliable S200x Pressure Relief Valve for Commercial Buildings and Municipal Water NetworksNegotiableMOQ: 1 Piece
-
Compact S200x Series Water Pressure Reducing Valve for HVAC and Fire Protection SystemsNegotiableMOQ: 1 Piece
-
S400X Flow Control Valve With High Precision Adjustment, Ideal for Water Supply NetworksNegotiableMOQ: 1 Piece
-
S400X Flow Control Valve for Building Services, Pressure Balancing and Flow RegulationNegotiableMOQ: 1 Piece
-
S400X Flow Control Valve for Water Treatment Plants, Corrosion-Resistant Stainless Steel OptionNegotiableMOQ: 1 Piece