Contact Platform Support
 Help Center
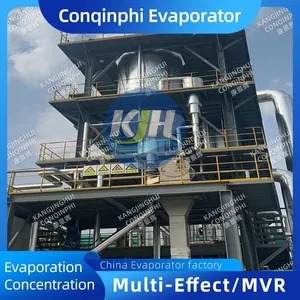
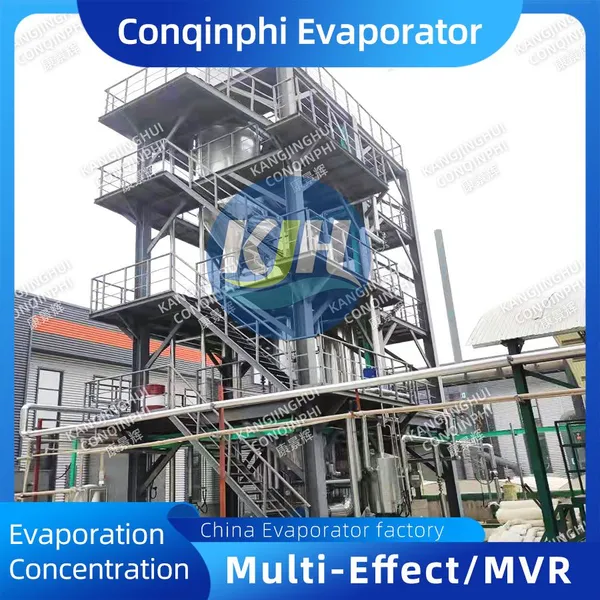
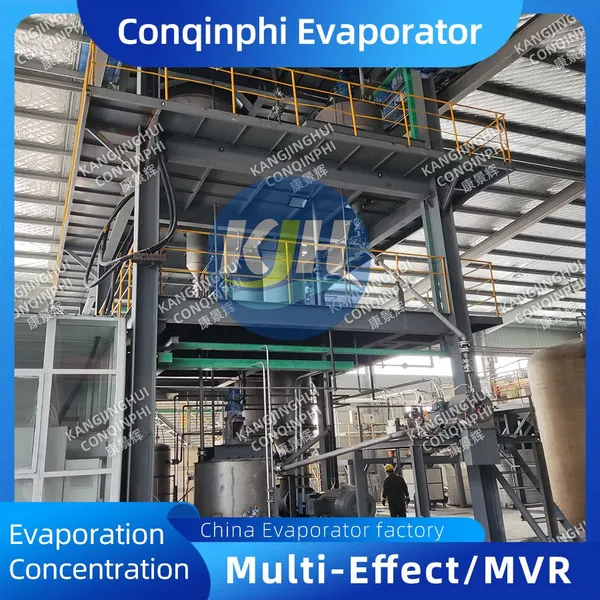
MVR Evaporator Unit for Zero Liquid Discharge (ZLD) Systems in Pharmaceutical Industry


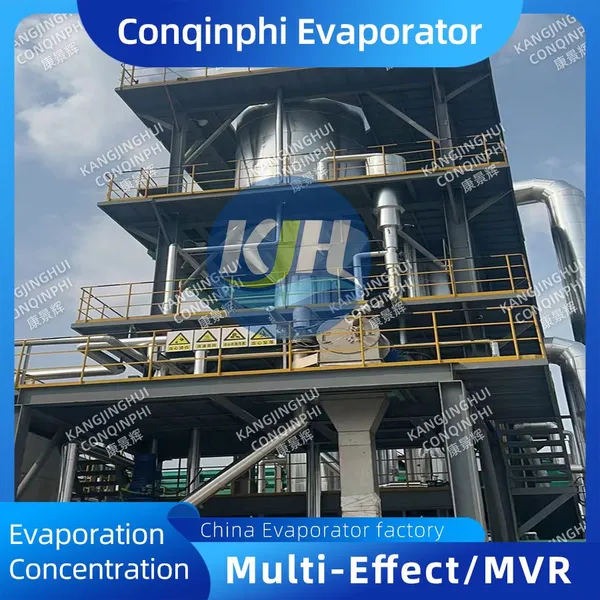
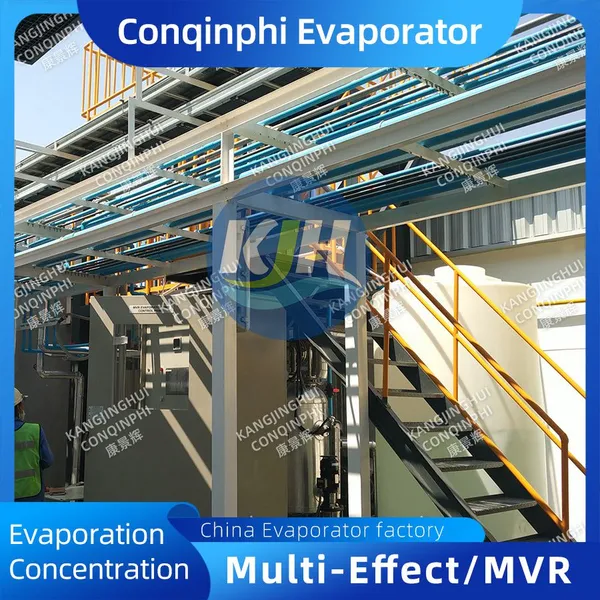
Product Spotlights




Related Products
-
 High-Efficiency MVR Evaporator Unit, 1000-5000 Kg/h Evaporation CapacityUS$ 52600MOQ: 1 Combo
-
MVR Evaporator Unit for Desalination Pretreatment and RO Brine ManagementUS$ 52600MOQ: 1 Combo
-
Customizable MVR Evaporator Unit With Mill Test Report and Performance GuaranteeUS$ 52600MOQ: 1 Combo
-
MVR Evaporator Unit With 12-Month Warranty and On-Site Technical SupportUS$ 52600MOQ: 1 Combo
-
Low Energy Consumption MVR Evaporator Unit With Heat Pump TechnologyUS$ 52600MOQ: 1 Combo
As a leading manufacturer specializing in advanced environmental solutions, Qingdao Conqinphi Environmental Technology Group Co., Ltd. is proud to present our high-performance MVR Evaporator Unit engineered specifically for Zero Liquid Discharge (ZLD) systems within the stringent pharmaceutical industry. With a modern factory spanning 10,000-30,000 square meters and a decade of expertise since our establishment in 2015, we deliver reliable, energy-efficient evaporation technology that helps pharmaceutical companies meet critical environmental compliance, recover valuable resources, and significantly reduce wastewater disposal costs.
Our MVR (Mechanical Vapor Recompression) Evaporator stands at the core of an effective ZLD strategy. It is designed to handle the complex and often variable wastewater streams generated from pharmaceutical production, including those containing salts, organic residues, and other dissolved solids. The system's primary function is to concentrate the wastewater into a minimal volume of solid residue or concentrated brine while producing high-purity distillate water suitable for reuse within the plant, thereby achieving "zero liquid discharge."
Key Features & Technical Advantages:
- Superior Energy Efficiency: The MVR technology recycles the latent heat of vaporization by mechanically compressing the generated vapor, raising its temperature, and reusing it as the primary heating source. This dramatically reduces steam consumption compared to traditional multi-effect evaporators, leading to significant operational cost savings.
- Tailored Pharmaceutical Design: We understand that pharmaceutical wastewater can be challenging, with components that may cause scaling, foaming, or corrosion. Our units are custom-designed based on a thorough analysis of your effluent. Material selection (such as SS316L or duplex steel for corrosive streams), choice of evaporator type (forced circulation for scaling-prone or viscous liquors, falling film for heat-sensitive components), and anti-foaming measures are all optimized for your specific application.
- Compact & Automated Operation: The integrated design results in a more compact footprint than conventional evaporation systems. Operation is managed by a sophisticated PLC-based automatic control system that ensures stable operation, optimizes energy use, and requires minimal manual intervention, enhancing safety and consistency.
- High-Quality Distillate Output: The system produces condensate water of exceptionally high purity, which can often be directly reused as cooling tower makeup, boiler feed water, or for other non-critical process applications, closing the water loop and reducing freshwater intake.
Core Technical Specifications:
The following table outlines typical design parameters and configurations. All specifications are customizable based on client requirements and feed analysis.
| Parameter | Description / Typical Range |
|---|---|
| Evaporation Capacity | Customizable from 1 to 100 tons of water evaporation per hour |
| Compressor Type | Integral gear centrifugal compressor or Turbo compressor (selected based on duty) |
| Heat Transfer Material | Titanium, 2205 Duplex, SS316, SS304 based on corrosion requirements |
| System Control | Fully automatic PLC with HMI, remote monitoring optional |
| Final Product | High-purity distillate and concentrated slurry/solid for disposal or recovery |
| Design Standards | Complies with cGMP considerations for pharmaceutical applications |
Benefits for Pharmaceutical Clients:
- Regulatory Compliance: Achieve and exceed stringent environmental regulations for wastewater discharge, avoiding fines and protecting your corporate reputation.
- Cost Reduction: Slash costs associated with off-site wastewater hauling and treatment. The low energy consumption of MVR technology directly lowers your utility bills.
- Sustainability Leadership: Implement a genuine circular economy solution by recovering water and, in some cases, crystallized salts, enhancing your site's sustainability profile.
- Operational Reliability: Our robust design, backed by comprehensive management systems including ISO9001 and ISO14000, ensures high availability and long service life with proper maintenance.
Trust in the proven capability of Qingdao Conqinphi. With an annual export value ranging between US$10-50 Million and a strong global presence across markets including North America, Europe, and Southeast Asia, we have demonstrated our ability to deliver complex environmental projects on an international scale. Our team of 201-300 dedicated professionals is committed to providing not just equipment, but a complete solution—from design and manufacturing to installation support. Choosing our MVR Evaporator for your pharmaceutical ZLD system means investing in a reliable, economical, and future-proof technology that aligns with both your environmental goals and bottom line. Contact us today to discuss your project requirements and receive a customized proposal.
Frequently Asked Questions (FAQ):
Q1: How does an MVR evaporator differ from a traditional multi-effect evaporator (MEE) for ZLD?
A: The primary difference lies in energy source. An MEE uses live steam in the first effect and cascades heat to subsequent effects. An MVR unit uses a mechanical compressor to recycle vapor from a single effect, compressing it to increase its temperature and reuse it as the heating medium. This makes MVR significantly more thermally efficient, though it requires electrical energy for the compressor.
Q2: Can your MVR system handle high-salinity or scaling-prone pharmaceutical wastewater?
A: Yes. For streams with high scaling potential, we typically recommend a Forced Circulation (FC) evaporator design. The high circulation velocity inside the tubes prevents salt deposition and scaling. Material selection and pre-treatment options are also considered to manage scaling and ensure stable, long-term operation.
Q3: What is the typical quality of the distilled water produced?
A: The condensate (distillate) quality is very high, typically with a conductivity of less than 10 µS/cm. It is suitable for reuse in many plant processes, such as cooling towers or boiler feedwater after possible polishing, drastically reducing freshwater consumption.
Q4: Is the system fully automatic?
A: Yes. Our standard package includes a fully automated PLC-based control system with a Human-Machine Interface (HMI). It controls all pumps, valves, the compressor, and monitors key parameters (pressure, temperature, level), allowing for unattended operation and easy data logging.
Q5: What kind of maintenance does the MVR compressor require?
A: The high-speed centrifugal compressors we use are designed for continuous industrial operation. Maintenance primarily involves regular monitoring of vibrations and bearing conditions, periodic oil changes (if oil-lubricated), and adherence to the manufacturer's service schedule. They are known for high reliability and long intervals between major services.
Q6: Can you integrate the MVR evaporator with our existing wastewater treatment train?
A: Absolutely. We provide customized engineering services. Our team can design the MVR unit to work seamlessly with your existing pre-treatment (like filtration, softening) or post-treatment (like crystallizers, dryers) systems to form a complete ZLD solution.
Q7: Do you offer pilot testing or treatability studies?
A: For critical applications or new wastewater compositions, we strongly recommend a treatability study. We can arrange for pilot-scale testing using a mobile unit or lab-scale equipment to gather precise design data and confirm process feasibility before full-scale investment.
Q8: What is the lead time for a standard unit?
A: Lead time depends on the capacity, material specifications, and customization level. A typical unit can have a manufacturing lead time of 4 to 8 months after design finalization and order confirmation. We provide detailed project schedules upon quotation.

Send Inquiry to This Supplier


You May Also Like
-
MVR Evaporator Unit for Fruit Juice Concentration and Dairy ProcessingUS$ 52600MOQ: 1 Combo
-
High-Efficiency MVR Falling Film Evaporator With Titanium Tubes for Corrosive LiquidsUS$ 42600 - 58000MOQ: 1 Combo
-
Compact MVR Falling Film Evaporator for Pharmaceutical and Food Grade ApplicationsUS$ 42600 - 58000MOQ: 1 Combo
-
Durable MVR Falling Film Evaporator With Comprehensive Technical Support and Spare Parts ServiceUS$ 42600 - 58000MOQ: 1 Combo
-
MVR Falling Film Evaporator With Mill Test Report and 18-Month Core Component WarrantyUS$ 42600 - 58000MOQ: 1 Combo
-
Reliable MVR Falling Film Evaporator With On-Site Installation and Operator Training IncludedUS$ 42600 - 58000MOQ: 1 Combo
-
MVR Falling Film Evaporator for Chemical and Salt Concentration With Standard Compliant DesignUS$ 42600 - 58000MOQ: 1 Combo
-
Industrial MVR Falling Film Evaporator for High-Concentration Wastewater TreatmentUS$ 42600 - 58000MOQ: 1 Combo
-
MVR Falling Film Evaporator System With PLC Control and 304 Stainless Steel ConstructionUS$ 42600 - 58000MOQ: 1 Combo
-
Custom-Designed MVR Falling Film Evaporator for Zero Liquid Discharge (ZLD) ProjectsUS$ 42600 - 58000MOQ: 1 Combo