Contact Platform Support
 Help Center
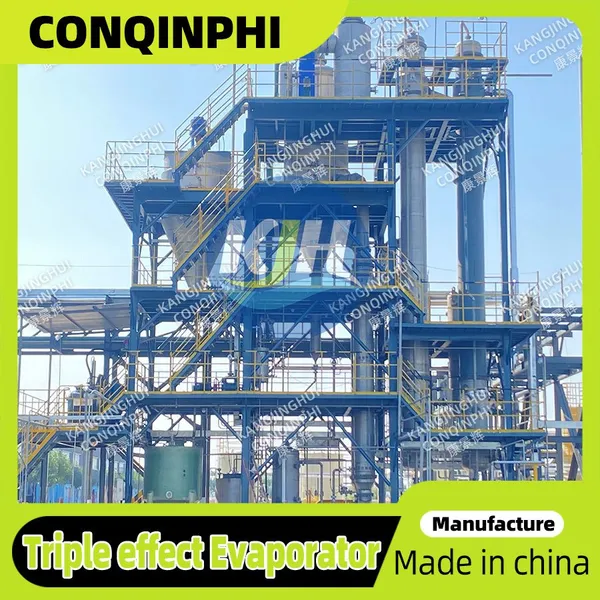
Industrial Heat Pump Distillation Column Unit, Explosion-Proof Design, IP65, 100L Capacity, PLC HMI Touch Screen





Product Spotlights




Related Products
-
 Semi-Automatic Heat Pump Distillation Column Unit, 316L Stainless Steel, 380V, 50L Processing Volume, Mill Test ReportUS$ 3290 - 859000MOQ: 1 Combo
-
PLC Controlled Heat Pump Distillation Column Unit, 304 Stainless Steel, 380V 50Hz, 150L/h CapacityUS$ 3290 - 859000MOQ: 1 Combo
-
Heat Pump Distillation Column Unit With Free Installation, 304 Stainless Steel, 380V, 12 Months Warranty, On-Site CommissioningUS$ 3290 - 859000MOQ: 1 Combo
-
Compact ZLD Treatment Unit With 98% Water Recovery Rate, Automated OperationUS$ 2180 - 1209000MOQ: 1 Combo
-
ZLD System for Chemical Manufacturing Plant, High Efficiency Evaporation and CrystallizationUS$ 2180 - 1209000MOQ: 1 Combo
Qingdao Conqinphi Environmental Technology Group Co., Ltd., established in 2015 with a factory spanning 10,000–30,000 square meters, brings you the Industrial Heat Pump Distillation Column Unit – a cutting-edge solution for solvent recovery and concentration processes. Designed with an explosion-proof enclosure, IP65 protection rating, and a PLC HMI touch screen, this 100L capacity unit combines safety, efficiency, and intuitive operation. Our team of 201–300 employees and annual export value of US$10–50 million ensure global-standard quality and reliable after-sales support.
Key Features & Technical Specifications
- Explosion-Proof Design: Built for hazardous environments, meeting ATEX/IECEx standards (optional). Ensures safe operation in volatile atmospheres.
- IP65 Protection: Dust-tight and protected against water jets, suitable for harsh industrial settings.
- 100L Capacity: Ideal for batch processing of solvents, essential oils, and chemical intermediates.
- PLC + HMI Touch Screen: User-friendly interface for real-time monitoring, parameter setting, and automated control. Supports remote connectivity.
- Heat Pump Technology: Energy-efficient heating and cooling, reducing operational costs by up to 40% compared to conventional electric heaters.
- High Precision Distillation: Glass column packing (optional) and temperature control within ±0.5°C ensure high-purity separation.
- Stainless Steel Construction: 304/316 SS for corrosion resistance and longevity. Customizable to meet specific chemical compatibility.
- Compact Footprint: Space-saving design with integrated condenser and receiver, minimizing floor space.
| Parameter | Specification |
|---|---|
| Capacity | 100L (batch), customizable from 50L to 500L |
| Heating Power | 12kW (heat pump) – efficient, adjustable |
| Temperature Range | Ambient – 200°C (controlled) |
| Pressure Range | Atmospheric to -0.095 MPa (vacuum optional) |
| Column Diameter | Ø150mm (customizable) |
| Material | SS304/316L, borosilicate glass column optional |
| Protection Class | IP65 (electric enclosure) |
| Control Interface | 7-inch HMI touch screen, PLC (Siemens or Mitsubishi) |
| Dimensions (L×W×H) | 1200×800×3000 mm (approx.) |
| Weight | Approx. 800 kg |
Customer Benefits
- Safety First: Explosion-proof and IP65 design minimizes risks in flammable environments, protecting personnel and assets.
- Energy Savings: Heat pump technology recycles thermal energy, reducing electricity consumption by 30–50% compared to traditional resistance heating.
- Easy Operation: PLC HMI touch screen allows one-button start, recipe management, and data logging. No specialized training required.
- High Purity Output: Precision temperature control and column packing enable recovery of solvents with purity >99%.
- Low Maintenance: Stainless steel construction and quality components ensure long service life with minimal downtime.
- Customizable: Options for vacuum operation, multiple column packings, and integration with existing lines.
Trusted by Global Markets
As a manufacturer with ISO9001, HACCP, SA8000, and OHSAS18001 certifications, Qingdao Conqinphi delivers consistent quality. Our products are exported to North America, South America, Europe, Southeast Asia, Africa, Oceania, and the Middle East. With a factory size of 10,000–30,000 m² and a dedicated R&D team, we can tailor the distillation column to your specific process requirements. We offer 24/7 technical support and a 12-month warranty against manufacturing defects. Contact us today for a customized solution.
Frequently Asked Questions
Q1: What is the explosion-proof rating of this unit?
A: The standard design meets IP65 and is compatible with ATEX/IECEx Zone 1 or Zone 2 environments. Specific certifications can be added upon request.
Q2: Can this unit handle high-viscosity liquids?
A: Yes, with optional agitation and heating jacket. Our team can recommend the best configuration for your material.
Q3: Is the PLC HMI touch screen available in multiple languages?
A: Yes, the interface supports English, Chinese, Spanish, and other languages on demand.
Q4: What is the typical payback period for energy savings?
A: Depending on usage, the heat pump system can reduce energy costs by up to 50%, achieving payback within 12–18 months.
Q5: Can I integrate the unit with my existing distillation column?
A: Yes, we provide adapters and customization for retrofitting. Contact our engineering team for a feasibility study.
Q6: What are the maintenance requirements?
A: Routine checks include cleaning the column packing, inspecting seals, and verifying sensor calibration. Full manual provided.
Q7: Do you offer training for operators?
A: Yes, we provide on-site training and remote video support as part of the commissioning package.
Q8: What is the lead time for a 100L unit?
A: Standard lead time is 30–45 days, depending on customization level. Rush orders are available.

Send Inquiry to This Supplier


You May Also Like
-
ZLD Wastewater Treatment Plant With Multi-Stage Evaporation and Crystallization, 50Hz/60HzUS$ 2180 - 1209000MOQ: 1 Combo
-
Automatic Zero Liquid Discharge Equipment With IP65 Waterproof Design and 10m3/h CapacityUS$ 2180 - 1209000MOQ: 1 Combo
-
304 Stainless Steel ZLD Wastewater Treatment System With PLC Control and 220V Power SupplyUS$ 2180 - 1209000MOQ: 1 Combo
-
PLC-Controlled Zero Liquid Discharge System for Industrial Wastewater, 304SS, 380VUS$ 2180 - 1209000MOQ: 1 Combo
-
Skid-Mounted Zero Liquid Discharge Equipment With 220V/380V, ISO Standard CompliantUS$ 2180 - 1209000MOQ: 1 Combo
-
Zero Liquid Discharge Wastewater Treatment for Pharmaceutical Industry, 304 Stainless SteelUS$ 2180 - 1209000MOQ: 1 Combo
-
Zero Liquid Discharge Equipment With 1 Year Warranty and On-Site Technical TrainingUS$ 2180 - 1209000MOQ: 1 Combo
-
Reliable ZLD Wastewater Treatment System With Free Maintenance and Spare Parts SupportUS$ 2180 - 1209000MOQ: 1 Combo
-
Zero Liquid Discharge System for Food Processing Wastewater, Hygienic Design, 304 Stainless Steel, 5 M³/h, Automatic Operation, 1 Year WarrantyUS$ 3210 - 879000MOQ: 1 Combo
-
Zero Liquid Discharge System for Chemical Plant, Heavy Duty Construction, 316 Stainless Steel, 20 M³/day, 380V, 50 HzUS$ 3210 - 879000MOQ: 1 Combo