


 Contact Platform Support
 Help Center
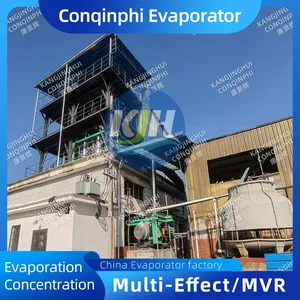
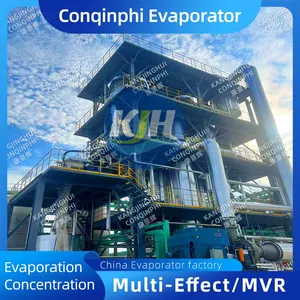
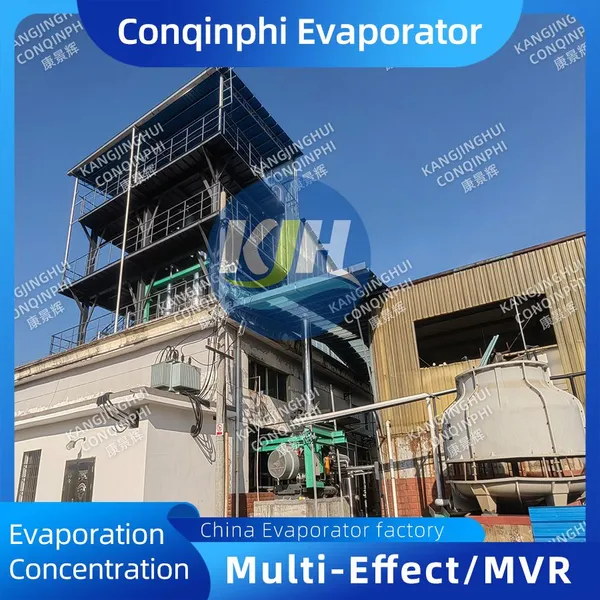
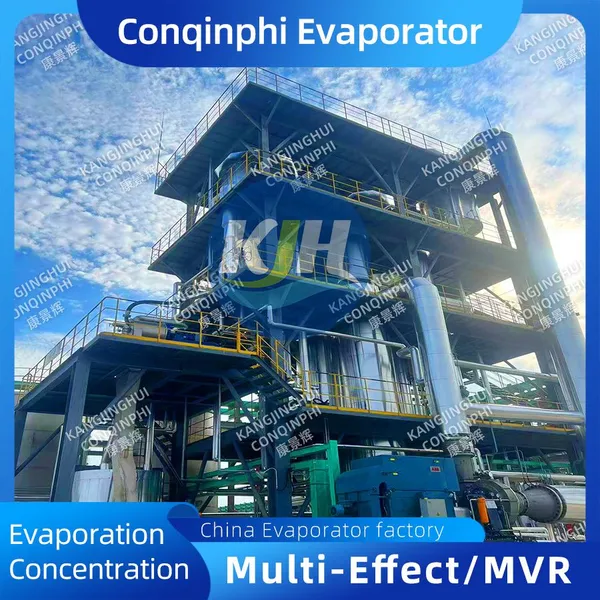
CONQINPHI Easy Maintenance Long Lifespan Energy Saving Mvr Evaporator for Liquid Purification







Product Spotlights




Related Products
-
 Innovative Mvr Evaporator With Advanced Vapor Recompression TechnologyUS$ 2840 - 551000MOQ: 1 Combo
-
Custom - Designed Wastewater Mvr Evaporator to Meet Specific RequirementsUS$ 3270 - 889000MOQ: 1 Combo
-
CONQINPHI Easy Maintenance Long Lifespan Energy Saving Mvr Evaporator for Liquid PurificationUS$ 2800 - 76900MOQ: 1 Combo
-
Conqinphi High Capacity Vacuum Mvr Evaporator for Large - Scale ProductionUS$ 2840 - 64900MOQ: 1 Combo
-
Conqinphi High Capacity Vacuum Mvr Evaporator for Large - Scale ProductionUS$ 2840 - 64900MOQ: 1 Combo
Qingdao Conqinphi Environmental Technology Group Co., Ltd. proudly presents our premium Vacuum Evaporator Concentrator for Sorbitol with a capacity of 1000 L/H and advanced PLC Touch Screen Control. As a dedicated manufacturer established in 2015, we specialize in designing and producing high-efficiency evaporation systems for the food, chemical, and pharmaceutical industries. This concentrator is engineered to deliver consistent, energy-saving performance in the concentration of sorbitol solutions, ensuring product purity and minimal thermal degradation. Our extensive factory spanning 10,000–30,000 square meters and our annual export value of US$10–50 million underscore our commitment to quality and global supply capability.
The core of this equipment lies in its vacuum evaporation technology, which lowers the boiling point of the liquid, allowing gentle concentration of heat-sensitive sorbitol at reduced temperatures. This preserves the functional properties and sweetness profile of the sorbitol while significantly reducing energy consumption. The integrated PLC touch screen control system provides intuitive operation, real-time monitoring, and automatic adjustment of parameters such as temperature, vacuum level, feed rate, and discharge concentration. Operators can easily program recipes, view trends, and set alarms, ensuring consistent batch-to-batch quality.
Key Features and Advantages
High Evaporation Efficiency – The specially designed heat exchanger and vacuum system achieve a high evaporation rate of up to 1000 L/H for water removal from sorbitol solutions.
Gentle Processing – Operating under vacuum (typically -0.08 to -0.095 MPa) allows evaporation at temperatures as low as 50–70°C, preventing discoloration or degradation of sorbitol.
PLC Touch Screen Control – User-friendly HMI with multi-language support, data logging, and remote monitoring capability (optional). Automatic control of valves, pumps, and heating source.
Customizable Configurations – Available in single-effect, double-effect, or multi-effect designs to optimize steam consumption. Heating by steam, thermal oil, or electric heater as per client requirement.
Robust Construction – Made of high-quality stainless steel (SUS304 or SUS316L) for corrosion resistance and compliance with food-grade standards. All product contact surfaces are polished to a mirror finish (Ra ≤ 0.4 μm).
Energy Saving – With an optional heat recovery system and intelligent control, the concentrator reduces steam consumption by 20–30% compared to traditional atmospheric evaporators.
Easy Maintenance – Quick-opening covers, CIP cleaning nozzles, and modular design minimize downtime and simplify sanitization.
Technical Specifications (Typical)
| Parameter | Value / Description |
|---|---|
| Evaporation Capacity | 1000 L/H (water removal) |
| Feed Concentration | Typically 30–50% (adjustable based on sorbitol property) |
| Final Concentration | Up to 85% (depending on viscosity and customer requirement) |
| Operating Vacuum | -0.085 MPa (customizable range) |
| Evaporation Temperature | 55–75°C (vacuum dependent) |
| Heating Source | Steam (0.3–0.6 MPa) / Electric (optional) / Thermal Oil |
| Power Supply | 380V / 50Hz (or as per local standard) |
| Control System | PLC + 10-inch Touch Screen (Siemens or Mitsubishi brand optional) |
| Material of Construction | SUS304 / SUS316L (product contact parts) |
| Dimensions (Approx.) | L6000 × W2500 × H4500 mm (customizable) |
Benefits for Your Production
Improved Product Quality – Low-temperature concentration maintains the natural properties of sorbitol, preventing caramelization or browning.
Higher Throughput – 1000 L/H capacity enables large-scale continuous or batch processing to meet your production demands.
Operator Convenience – The PLC touch screen reduces manual intervention, minimizes human error, and provides historical data for traceability.
Reduced Operating Costs – Intelligent automation optimizes steam and energy usage, lowering your overall cost per liter of concentrate.
Flexibility – The system can be adapted for other liquid food or chemical products with similar viscosity and heat sensitivity, such as fruit juice, milk, or glucose syrup.
At Qingdao Conqinphi Environmental Technology Group, we adhere to rigorous quality management systems. Our factory is certified under ISO9001, ISO14000, HACCP, and OHSAS18001 among other standards, ensuring that every concentrator meets international safety and performance benchmarks. With a team of over 200 skilled employees and a strong presence in markets across North America, Europe, Southeast Asia, and Africa, we have the expertise to deliver turnkey solutions tailored to your specific sorbitol concentration needs.
We offer comprehensive after-sales support including installation guidance, commissioning, operator training, and spare parts supply. Our Qingdao port location facilitates efficient global logistics. Contact us today to discuss your requirements or request a detailed quotation. Let our Vacuum Evaporator Concentrator elevate your sorbitol production to new levels of efficiency and quality.
Frequently Asked Questions
Q: What is the maximum concentration of sorbitol achievable with this evaporator?
A: The final concentration can reach up to 85% solids, depending on the initial feed concentration and viscosity of the sorbitol. Custom adjustments can be made to reach higher levels if required.Q: Can this equipment handle other types of sugar alcohols or sweeteners?
A: Yes, the same vacuum evaporator design is suitable for concentrating other sugar alcohols like maltitol, xylitol, and erythritol, as well as liquid glucose and fructose syrups. Parameter changes can be programmed via the PLC.Q: What is the typical power consumption and steam usage?
A: For a single-effect configuration, steam consumption is approximately 0.4–0.5 kg of steam per kg of water evaporated. Power consumption for pumps and control system is typically under 15 kW. Exact numbers depend on your specific operating conditions.Q: Is the PLC touch screen available with remote monitoring and data export?
A: Yes, we can integrate Ethernet or Wi-Fi modules for remote access, and the HMI supports USB data export to CSV or Excel for production records and analysis.Q: What materials are used for the evaporator body and heat exchanger?
A: Standard construction is SUS304 stainless steel. For applications requiring higher corrosion resistance (e.g., acidic or saline conditions), we offer SUS316L as an optional upgrade.Q: How long does installation and commissioning take?
A: On-site installation and commissioning typically take 5–7 working days, provided that utilities (steam, electricity, water, drain) are prepared. We also provide remote guidance and on-site training for your operators.Q: Do you provide customized designs for different capacity requirements?
A: Absolutely. We have a range of standard models from 200 L/H to 10,000 L/H, and we can customize the evaporator to match your exact throughput, space constraints, and automation preferences.Q: What kind of warranty and after-sales support do you offer?
A: We offer a 12-month warranty against manufacturing defects, with lifetime technical support. Spare parts are readily available, and our service team can respond to inquiries within 48 hours.

Send Inquiry to This Supplier


You May Also Like
-
Conqinphi - Response Mvr Evaporator for Rapid Liquid EvaporationUS$ 2840 - 64900MOQ: 1 Combo
-
Custom - Designed Wastewater Mvr Evaporator to Meet Specific RequirementsUS$ 3270 - 66270MOQ: 1 Combo
-
Conqinphi SS316L Multiple-Effect Vacuum Evaporator for Edible Oil ConcentrationUS$ 3270 - 66270MOQ: 1 Combo
-
Advanced - Technology Mvr Evaporator System for Modern IndustriesUS$ 3160 - 24800MOQ: 1 Combo
-
Conqinphi Stable - Running Mvr Evaporator for Industrial WastewaterUS$ 3270 - 66270MOQ: 1 Combo
-
High - Precision Mvr Evaporator for Accurate Concentration ResultsUS$ 88300 - 8890000MOQ: 1 Combo
-
Innovative Mvr Evaporator With Advanced Vapor Recompression TechnologyUS$ 88300 - 8890000MOQ: 1 Combo
-
Falling Film Shell and Tube Evaporator for Chemical WastewaterUS$ 4600 - 315000MOQ: 1 Combo
-
Conqinphi MVR Evaporator for Xylitol Solution ConcentrationUS$ 7280 - 769000MOQ: 1 Combo
-
Conqinphi Acid-Proof Alkali-Resistant Forced-Circulation Multi-Effect EvaporatorUS$ 5470 - 878700MOQ: 1 Combo


