Contact Platform Support
 Help Center
MVR Crystallization Evaporator for Sodium Sulfate Recovery in Textile Wastewater Treatment




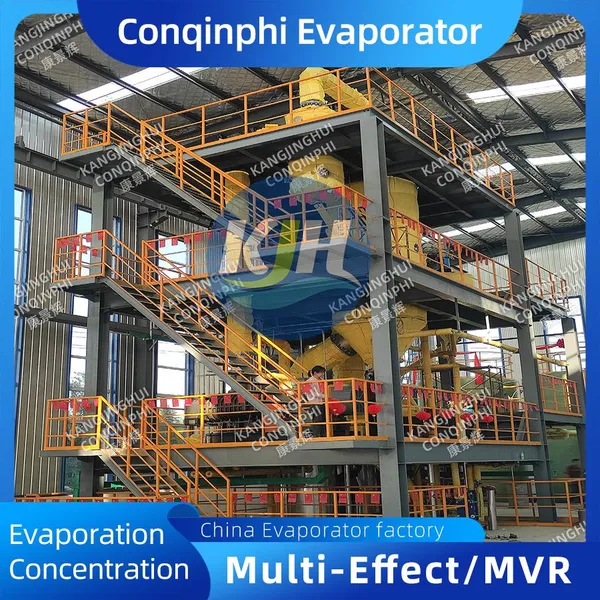
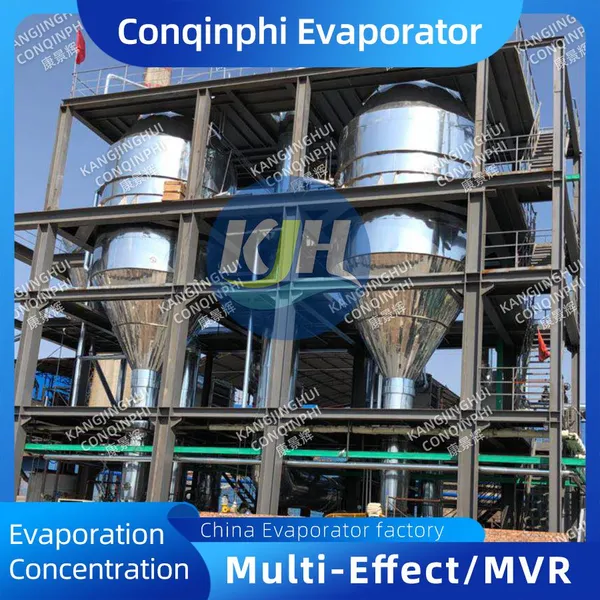
Product Spotlights




Related Products
-
 Compact MVR Crystallization Evaporator Semi-Auto 50Hz 380V for Small Scale Chemical ProcessingUS$ 4150 - 89000MOQ: 1 Set
-
MVR Evaporator Used in Food Processing - Fruit Juice Concentration With Low Temperature Evaporation and CIPUS$ 73800 - 805000MOQ: 1 Combo
-
Compact MVR Mechanical Vapor Recompression Evaporator 316L Stainless Steel With Touch Screen PLC ControlUS$ 73800 - 805000MOQ: 1 Combo
-
MVR Concentration Evaporator for Pharmaceutical Industry - Crystallization and Solvent Recovery Low TemperatureUS$ 73800 - 805000MOQ: 1 Combo
-
MVR Concentration Evaporator 1000L/H 304 Stainless Steel Shell and Tube Heat Exchanger Automatic OperationUS$ 73800 - 805000MOQ: 1 Combo
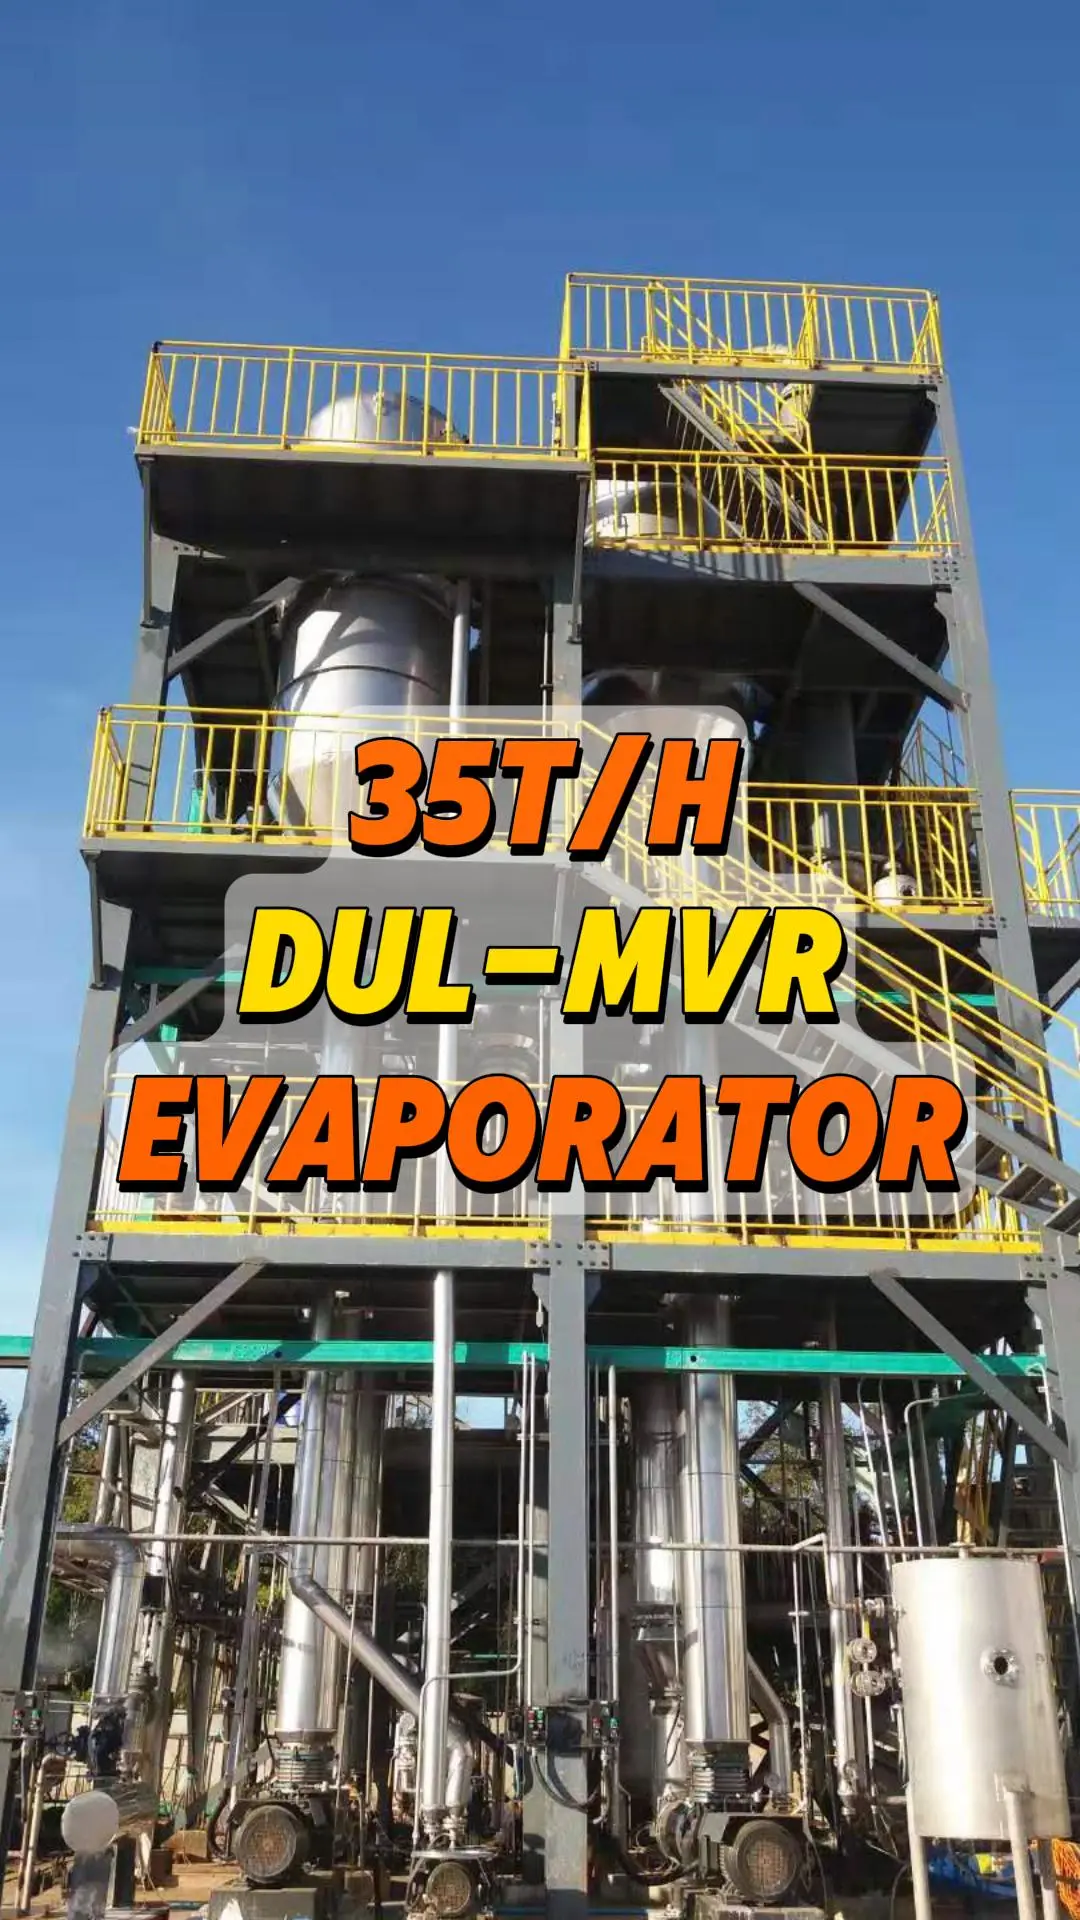
Qingdao Conqinphi Environmental Technology Group Co., Ltd. presents our advanced MVR Crystallization Evaporator for Sodium Sulfate Recovery in Textile Wastewater Treatment. As a leading manufacturer established in 2015 with a factory spanning 10,000-30,000 square meters and over 200 skilled employees, we bring years of expertise in industrial wastewater solutions. This MVR (Mechanical Vapor Recompression) evaporator is designed specifically for textile dyeing and finishing wastewater containing high concentrations of sodium sulfate, offering a cost-effective and energy-efficient method to recover valuable salt while achieving zero liquid discharge (ZLD). By combining evaporation and crystallization in a single integrated system, our equipment helps textile factories reduce waste, lower operating costs, and meet stringent environmental regulations.
Our MVR Crystallization Evaporator leverages mechanical vapor recompression technology to dramatically reduce energy consumption. Instead of using live steam to heat the feed, the system compresses the vapor generated during evaporation, raising its temperature and pressure, then recycles that heat back into the process. This closed-loop design cuts steam usage by up to 60-80% compared to traditional multi-effect evaporators, making it an ideal choice for facilities aiming to improve sustainability and profitability. The result is a highly efficient, compact, and automated solution for sodium sulfate recovery from textile wastewater.
Product Features & Advantages
- Energy Efficiency: Only requires electrical power for the compressor – typical specific energy consumption is as low as 20-50 kWh per ton of water evaporated, significantly lower than conventional evaporators.
- High Quality Crystal Output: Controlled crystallization conditions (temperature, supersaturation, residence time) produce sodium sulfate decahydrate (Glauber salt) or anhydrous salt with >99% purity, which can be reused in the dyeing process or sold as a byproduct.
- Fully Automatic Operation: PLC-based control with HMI touchscreen enables unattended running, real-time monitoring of temperature, pressure, level, and concentration, plus automatic start/stop and alarm functions.
- Robust Material Construction: All wetted parts are made from SS316L stainless steel or duplex stainless steel, providing excellent corrosion resistance against sulfate solutions at elevated temperatures (up to 120°C).
- Compact Footprint: Vertical falling film or forced circulation design minimizes floor space requirements, ideal for retrofitting into existing treatment facilities.
- Versatile Feed Pre-treatment: Integrated options for pH adjustment, filtration, and decolorization ensure stable operation even with fluctuating wastewater quality.
Technical Specifications (Typical)
| Parameter | Value / Range |
| Evaporation Capacity | 1 – 100 tons water/day (customizable) |
| Energy Consumption | 20 – 50 kWh/ton water evaporated |
| Operating Temperature | 60 – 110 °C (adjustable) |
| Maximum Salt Concentration in Feed | Up to 25% (w/w) Na₂SO₄ |
| Crystal Purity | ≥99% (anhydrous or decahydrate) |
| Compressor Type | Centrifugal or Roots (oil-free option) |
| Material (wetted parts) | SS316L / Duplex SS2205 |
| Control System | PLC + HMI (Siemens or equivalent) |
Customer Benefits
- Lower Operating Costs: Reduced steam consumption and electricity-only operation slash energy expenses. Typical payback period is 1-2 years based on energy savings and recovered salt value.
- Environmental Compliance: Achieve zero liquid discharge (ZLD) and meet wastewater discharge standards (e.g., GB 4287-2012 for textile industry). Recovered water can be recycled, reducing freshwater intake.
- Revenue from Byproduct: High-purity sodium sulfate crystals can be sold to detergent, glass, or paper industries, turning waste into profit.
- Minimal Maintenance: Fewer moving parts than multi-effect systems, with easy access for cleaning and inspection. Anti-scaling design reduces fouling.
- Reliable After-Sales Support: Qingdao Conqinphi offers full engineering, installation supervision, commissioning, and training services.
Choose Conqinphi for proven expertise. Our factory, certified under ISO9001, ISO14001, and OHSAS18001 management systems, delivers consistent quality. With an annual export value between US$10-50 million, we serve markets across North America, South America, Europe, Southeast Asia, Africa, and Oceania. Our team of over 200 professionals includes experienced R&D engineers who tailor each MVR system to specific wastewater characteristics. Thousands of successful installations worldwide attest to our reliability.
Contact us today for a free feasibility study and quotation. Let our MVR Crystallization Evaporator transform your textile wastewater treatment from a cost center into a value driver. We provide detailed process design, performance guarantees, and comprehensive support from Qingdao port.
Frequently Asked Questions (FAQ)
-
Q: What is the typical energy saving of an MVR evaporator compared to a multi-effect evaporator?
A: MVR systems can reduce energy consumption by 60-80% because they recycle latent heat of vaporization. Instead of consuming steam, they only need electricity for the compressor – typically 20-50 kWh per ton of water evaporated. -
Q: Can this system handle other salts besides sodium sulfate?
A: While designed primarily for sodium sulfate recovery from textile wastewater, the MVR technology can be adapted for other sulfate salts (e.g., magnesium sulfate) or chloride salts by adjusting crystallization parameters. Please consult our engineers for specific applications. -
Q: What is the maximum size (capacity) you offer?
A: We provide units from 1 ton/day pilot-scale to 100 tons/day industrial-scale. Larger capacities can be achieved by installing multiple trains. -
Q: How do you prevent scaling and fouling in the evaporator and crystallizer?
A: Our design incorporates anti-scaling measures such as controlled supersaturation, forced circulation, and periodic flushing. Optionally, we can integrate a seed crystal dosing system or magnetic treatment. Stainless steel construction also resists scaling. -
Q: What is the typical delivery time for a custom MVR crystallization evaporator?
A: After receiving detailed wastewater analysis and required capacity, we typically deliver within 4-6 months, including engineering, fabrication, testing, and shipping from Qingdao port. Expedited schedules are available for standard modules. -
Q: Does your company offer installation and commissioning assistance?
A: Yes, we provide on-site supervision of installation, startup, and commissioning by our experienced engineers. We also offer operator training and optional maintenance contracts. -
Q: What certifications do your products hold?
A: Our manufacturing processes are certified under ISO9001, ISO14001, and OHSAS18001. Additionally, we can design to meet CE, ASME, or other international standards upon request. -
Q: Can the recovered sodium sulfate be directly reused in textile dyeing?
A: Yes, with our controlled crystallization, the purity typically exceeds 99%, meeting the quality requirements for reuse as a dyeing auxiliary. A small portion of the recovered salt may need to be blended with fresh salt depending on the customer’s specific color sensitivity.

Send Inquiry to This Supplier


You May Also Like
-
MVR Concentration Evaporator Standard Compliant With Installation Training and After-Sales ServiceUS$ 73800 - 805000MOQ: 1 Combo
-
Skid-Mounted MVR Concentration Evaporator 10Bar Max Pressure Auto Control Valve for Zero Liquid DischargeUS$ 73800 - 805000MOQ: 1 Combo
-
304 Stainless Steel MVR Concentration Evaporator With PLC Control and Automatic Operation for Industrial WastewaterUS$ 73800 - 805000MOQ: 1 Combo
-
Reliable MVR Concentration Evaporator With 1-Year Warranty and Mill Test Report Factory Direct SupportUS$ 73800 - 805000MOQ: 1 Combo
-
Industrial MVR Evaporator System With CIP Cleaning Unit 3-Phase 380V High Efficiency for Chemical RecoveryUS$ 73800 - 805000MOQ: 1 Combo
-
Automatic MVR Concentration Evaporator 220V 50Hz Low Energy Consumption 500L/H Capacity 304 SSUS$ 73800 - 805000MOQ: 1 Combo
-
PLC Controlled Tube-type Skid-mounted MVR Evaporator, 304 Stainless Steel, 500L/h Evaporation Capacity for Industrial WastewaterUS$ 27500 - 639000MOQ: 5 Combos
-
High Vacuum Tube-type Skid-mounted MVR Evaporator, Operating Temperature up to 130°C, Continuous 24/7 DutyUS$ 27500 - 639000MOQ: 5 Combos
-
Tube-type Skid-mounted MVR Evaporator With IP55 Electrical Cabinet, Programmable Logic Controller, 380V 50HzUS$ 27500 - 639000MOQ: 5 Combos
-
Tube-type Skid-mounted MVR Evaporator With 1-year Warranty, On-site Installation Guidance and Operator Training IncludedUS$ 27500 - 639000MOQ: 5 Combos