


 Contact Platform Support
 Help Center
Purified Industrial Chlorine Gas for Water Treatment Disinfection


Product Spotlights


Related Products
-
 Chlor-Alkali Process Caustic Soda for Chemical & Water TreatmentUS$ 200000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Process Liquid Chlorine for Disinfection & SynthesisUS$ 200000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Process Hydrochloric Acid for Metal Pickling & Chemical ProcessingUS$ 200000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Plant EPC Project | Turnkey Solution for Caustic Soda & Hydrochloric Acid ProductionUS$ 100000 - 2000000MOQ: 1 Set
-
99% Caustic Soda Flakes EPC Project | Turnkey Industrial Solid NaOH Production PlantUS$ 100000 - 2000000MOQ: 1 Set
1 Product Overview
Liquid chlorine is a high-purity concentrated industrial chemical derived from the chlor-alkali electrolysis process, and it is one of the most fundamental and core chlorine-based raw materials in the modern chemical industry. Under sealed industrial conditions, purified gaseous chlorine is converted into yellow-green transparent liquid after low-temperature compression and liquefaction, namely industrial liquid chlorine.
Compared with ordinary gaseous chlorine, liquid chlorine boasts higher concentration, easier storage, lower transportation costs and stable chemical activity. Subjected to multi-stage impurity removal, drying, compression and precision liquefaction, this product features extremely low moisture and impurity content and reaches premium industrial grade standards. It possesses strong oxidation, sterilization and bleaching capacity, and can be used in diverse scenarios including chemical synthesis, industrial water treatment, papermaking bleaching, environmental disinfection and fine chemical processing. As a core derivative of the chlor-alkali industry, high-purity liquid chlorine serves as an indispensable basic raw material for large-scale industrial manufacturing and environmental treatment projects worldwide.
2 Technical Principle
The production of industrial liquid chlorine adopts chlor-alkali electrolysis gas purification + low-temperature compression liquefaction technology, a mature and standardized green production process widely used in the modern chlor-alkali sector. The whole process takes refined saturated brine as the sole raw material without adding hazardous chemical additives.
Firstly, saturated refined brine undergoes electrolysis inside an ion-exchange membrane electrolyzer to generate crude chlorine gas. Containing moisture, brine mist and trace impurities, crude chlorine gas is delivered to a multi-stage purification and drying system for dehumidification, dust removal and impurity filtration to obtain dry high-purity chlorine gas. Afterwards, pure gaseous chlorine is pressurized by a dedicated chlorine compressor and sent to the low-temperature liquefaction unit. In a sealed environment with constant temperature and pressure, gaseous chlorine completes physical phase transition and is fully condensed into high-purity liquid chlorine. Qualified liquid chlorine products are obtained via precision filtration, static settling and quality inspection, then stored in sealed pressure storage tanks. The whole production process adopts fully closed automatic control to guarantee stable product purity and zero external pollution discharge.
3 Main Features
Ultra-High Purity with Minimal Impurities: Supported by multi-stage drying, purification and precision liquefaction processes, finished liquid chlorine contains very low moisture and impurities without heavy metal residues. It features stable and reliable quality and meets the application standards of high-end industrial raw materials.
High Concentration & Robust Activity : Concentrated by low-temperature compression and liquefaction, liquid chlorine achieves greatly elevated chlorine concentration and stable molecular activity. It delivers efficient oxidation, sterilization and bleaching effects and enables sufficient and rapid reactions in various industrial applications.
Convenient Storage & Transportation: The liquid form drastically reduces volume for storage and transportation. It can be stably stored in sealed pressure vessels for a long time and supports long-distance transportation and mass industrial supply to satisfy demands of large-scale production.
Stable Chemical Properties: Precision process control throughout production ensures stable physical and chemical properties of liquid chlorine. It resists abnormal volatilization and deterioration, and maintains consistent reaction efficiency under diverse industrial working conditions.
High Safety & Full Compliance: Produced on fully closed automatic production lines with standardized pressure-resistant, low-temperature and anti-corrosion treatment. It complies with international specifications for chemical transportation and industrial usage safety.
Wide Industrial Compatibility: With outstanding oxidation, sterilization and bleaching performance, it adapts to diversified industrial scenarios such as chemical synthesis, industrial disinfection and papermaking bleaching with extensive coverage of applications.
4 Core Advantages
Process Advantage: Mature Chlor-Alkali Industrial Technology: Equipped with advanced ion-exchange membrane chlor-alkali electrolysis and low-temperature liquefaction technology, the production process is mature and stable. Product quality far exceeds ordinary crude chlorine products with high batch stability and low failure risk.
Quality Advantage: Strict Purification Control: Multi-stage purification, drying and filtration are implemented from crude gas generation to finished product delivery. Every batch of liquid chlorine undergoes comprehensive testing covering purity, moisture and impurities to eliminate quality fluctuation and improve yield of industrial finished products.
Cost Advantage: High Resource Utilization Rate: Closed-loop recycling of chlor-alkali by-products is realized with high brine conversion rate and low overall energy consumption. High-purity liquid chlorine achieves high utilization efficiency in industrial applications, effectively cutting enterprises’ raw material procurement and operating costs.
Application Advantage: Diversified Industrial Value: Integrating functions of chemical synthesis, high-efficiency sterilization and industrial bleaching, it fulfills differentiated raw material requirements of multiple industries and delivers high comprehensive value for multi-scenario industrial production.
Supply Advantage: Stable Mass Production Capacity: Supported by large-scale automatic chlor-alkali production lines, continuous, stable and mass supply is available. Standard tank truck transportation and customized packaging are supported to satisfy long-term large order demands of enterprises.
5 Core Production Components
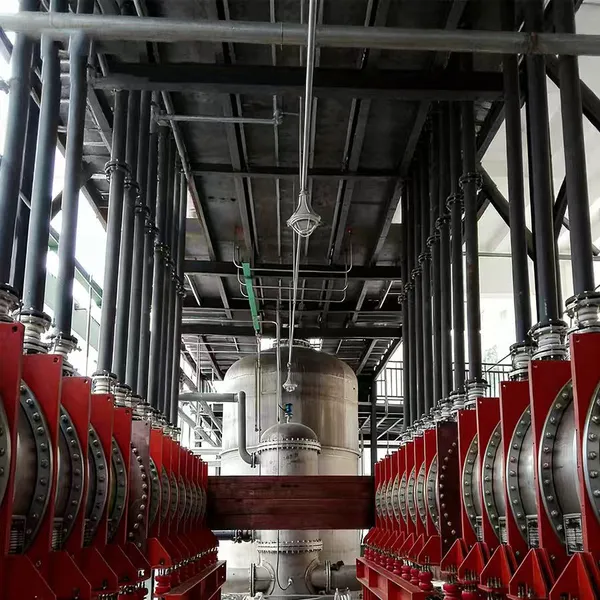
Ion-Exchange Membrane Electrolyzer: The core reaction equipment for liquid chlorine production. It electrolyzes refined saturated brine to produce crude chlorine gas with high electrolysis efficiency, stable gas output and long service life, providing sufficient high-quality raw gas for subsequent procedures.
Multi-Stage Chlorine Purification & Drying System: Professional impurity removal and dehumidification equipment that thoroughly eliminates brine mist, moisture and particulate impurities in crude chlorine gas to produce dry pure chlorine gas qualified for liquefaction.
Chlorine Compressor Unit: Specialized industrial pressurization equipment used to stabilize and boost pressure of purified chlorine gas to meet pressure requirements of the low-temperature liquefaction process.
Low-Temperature Liquefaction System: Core phase-change equipment for liquid chlorine formation. It creates a constant low-temperature environment to realize full condensation and liquefaction of gaseous chlorine into high-purity liquid chlorine.
Precision Filtration & Static Settling Device: Used for fine filtration and static purification of liquefied chlorine to remove trace residual impurities and further improve product purity and storage stability.
Sealed Storage & Testing Unit: Consists of anti-corrosion pressure storage tanks and professional quality inspection instruments, realizing safe storage, batch sampling inspection and standardized delivery of finished liquid chlorine.
6 Application Fields
Chemical Synthesis Industry: Serving as the core chlorine raw material for synthesis of hydrochloric acid, sodium hypochlorite, chlorinated paraffin, pesticide intermediates and various fine chemical products, it is widely adopted in inorganic and organic chemical production.
Environmental Protection & Water Treatment Industry: Applied for sterilization, algae removal and oxidative degradation of organic pollutants in municipal tap water, industrial circulating water and reclaimed water to ensure water quality safety and compliant discharge.
Papermaking & Textile Industry: Used for pulp bleaching in papermaking and fiber bleaching & purification in textile manufacturing to improve product whiteness and surface quality.
Pharmaceutical Industry: Utilized for synthesis of chlorine-containing pharmaceutical intermediates and preparation of medical disinfection raw materials, satisfying high-purity raw material standards for pharmaceutical production.
Metallurgy & Electroplating Industry: Suitable for auxiliary treatment of metal ore smelting and purification of electroplating solutions, acting as an important auxiliary raw material for metallurgical processing.
Daily Chemical & Disinfection Industry: Deployed for manufacturing various disinfectants, bleaching agents and daily chemical additives, delivering core raw materials for public health disinfection and daily chemical production.
Boasting 25 years of professional industry experience in production and supply, ZLN factory delivers premium,cost-effective chemical products with reliable quality. Equipped with fully automatic production systems and scientific modular production line design, we achieve stable output, high efficiency and low energy consumption while strictly complying with industrial standards. Different from ordinary manufacturers, ZLN provides flexible customized services tailored to diverse customer needs on product specifications, packaging and solutions. With direct factory pricing and optimized production processes, we help clients cut procurement costs and obtain high-quality, stable chemical supplies with comprehensive professional support.

Send Inquiry to This Supplier


You May Also Like
-
33% Hydrochloric Acid Equipment | Corrosion Resistant Industrial HCl Production Plant SystemUS$ 100000 - 2000000MOQ: 1 Set
-
Liquid Chlorine Equipment | Industrial Liquid Chlorine Production, Storage & Handling SystemUS$ 100000 - 2000000MOQ: 1 Set
-
Ion Membrane Chlor-Alkali Plant EPC Turnkey ProjectUS$ 100000 - 2000000MOQ: 1 Set
-
99% High Purity Caustic Soda Flakes EPC Turnkey LineUS$ 100000 - 2000000MOQ: 1 Set
-
31% Industrial Grade Hydrochloric Acid Synthesis EquipmentUS$ 100000 - 2000000MOQ: 1 Set
-
Industrial Liquid Chlorine Complete EquipmentUS$ 100000 - 2000000MOQ: 1 Set
-
Custom Chlor-Alkali Plant EPC Turnkey Solution for Integrated Chemical Manufacturing PlantUS$ 100000 - 2000000MOQ: 1 Set
-
99% Caustic Soda Flakes EPC Turnkey Plant for Industrial ManufacturingUS$ 100000 - 2000000MOQ: 1 Set
-
33% Hydrochloric Acid Production Equipment for Industrial Neutralization & PicklingUS$ 100000 - 2000000MOQ: 1 Set
-
Industrial Liquid Chlorine Processing Equipment for Chemical ManufacturingUS$ 100000 - 2000000MOQ: 1 Set


