


 Contact Platform Support
 Help Center
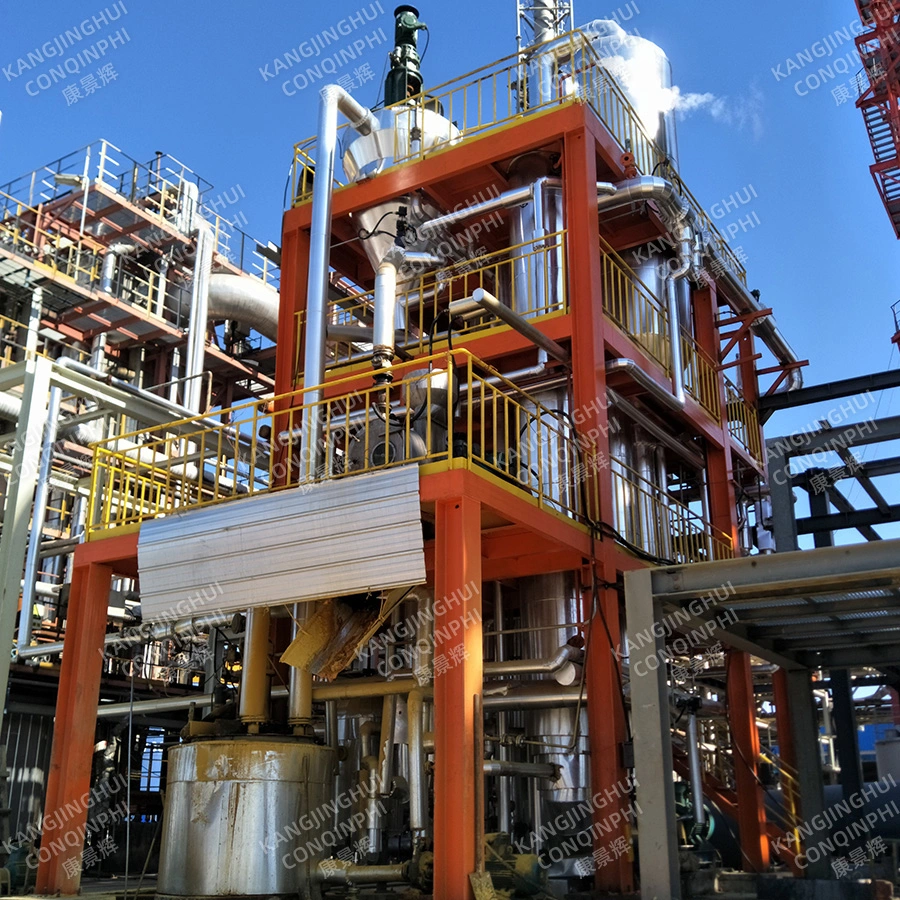
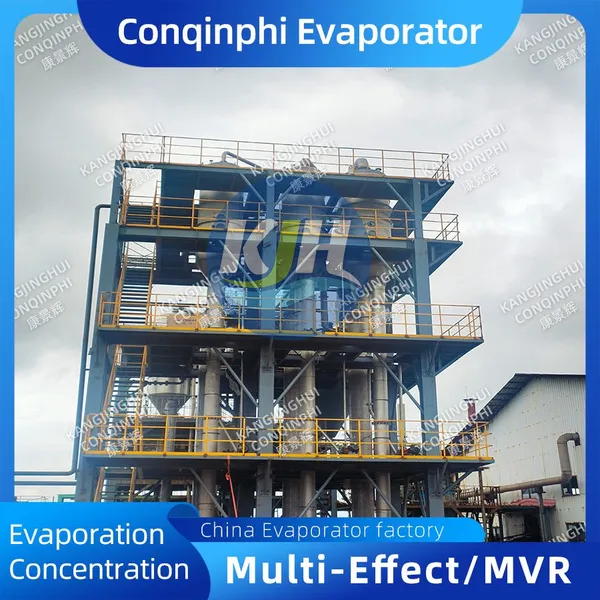
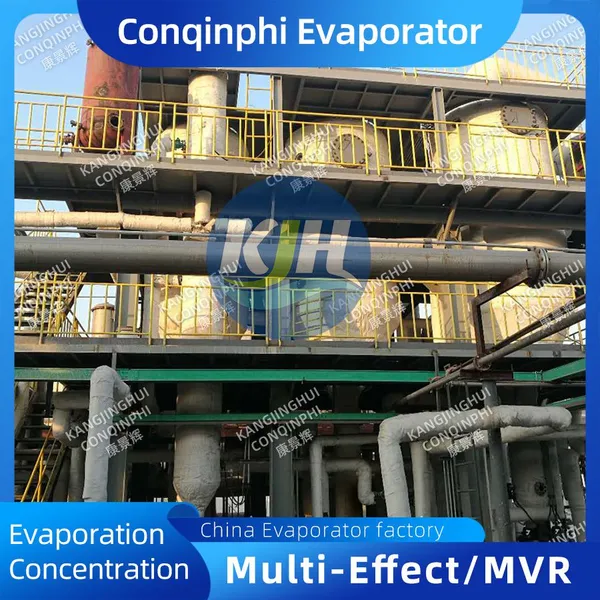
For Dairy Industry: Long Tube Vertical Evaporator for Milk Concentration, 304 SS, PLC Controlled




Product Spotlights




Related Products
-
 304 Stainless Steel Long Tube Vertical Evaporator With PLC Control for Efficient ConcentrationUS$ 21200 - 879000MOQ: 1 Combo
-
Long Tube Vertical Evaporator With 1-Year Warranty and On-Site Installation TrainingUS$ 21200 - 879000MOQ: 1 Combo
-
Industrial MVR Sodium Chloride Crystallizer With Forced Circulation, 316L Material, 220V/50Hz Power SupplyUS$ 3220 - 7859000MOQ: 1 Combo
-
Energy Saving 30% MVR Evaporator for NaCl Crystallization With 85°C Operating Temperature and Automatic ControlUS$ 3220 - 7859000MOQ: 1 Combo
-
Mill Test Report Included – MVR Evaporator Crystallizer for Sodium Chloride With After Sales Support and Spare PartsUS$ 3220 - 7859000MOQ: 1 Combo
Welcome to Qingdao Conqinphi Environmental Technology Group Co., Ltd. – a professional manufacturer with over 8 years of expertise in industrial evaporation systems. Our Long Tube Vertical Evaporator for Milk Concentration is specifically engineered to meet the stringent demands of the dairy processing industry. Constructed from high-quality 304 Stainless Steel and equipped with a state-of-the-art PLC control system, this evaporator delivers exceptional efficiency, precise temperature management, and reliable operation for concentrating milk and other dairy liquids.
With a factory spanning 10,000–30,000 square meters and an annual export value exceeding US$10 million, we have supplied advanced evaporation solutions to clients across North America, Europe, Southeast Asia, and the Middle East. Our equipment is designed to enhance product quality while reducing energy consumption and operational costs. Whether you need to concentrate whole milk, skim milk, whey, or other dairy products, our Long Tube Vertical Evaporator provides a robust, hygienic, and customizable solution tailored to your production capacity.
Below we present detailed product features, technical specifications, and advantages that make this evaporator a trusted choice for dairy manufacturers worldwide.
Key Product Features
- Superior Material Construction: All product contact parts are made of 304 Stainless Steel, ensuring excellent corrosion resistance, easy cleaning, and compliance with dairy hygiene standards.
- PLC Controlled Automation: The integrated Programmable Logic Controller (PLC) provides precise control over temperature, vacuum level, feed rate, and concentration ratio. It enables automatic start-up, shut-down, and real-time monitoring, reducing manual intervention and human error.
- Long Tube Vertical Design: The vertical tube arrangement offers a larger heat transfer area in a compact footprint, efficient use of floor space, and excellent liquid distribution, resulting in uniform concentration and minimal fouling.
- Energy Efficient Operation: Optional vapor recompression (thermal or mechanical) can be integrated to reuse latent heat, significantly lowering steam consumption. The evaporator is designed for low-temperature evaporation under vacuum, preserving milk proteins and nutrients.
- Customizable Evaporation Capacity: Available in a range from 500 kg/h to 5,000 kg/h (and higher upon request), the system can be scaled to match your production line requirements.
- Hygienic Design & Easy Maintenance: Smooth surfaces, CIP (Clean-in-Place) compatibility, and quick-disconnect fittings minimize downtime and ensure thorough sanitation between batches.
- Remote Monitoring & Data Logging: The PLC system can be connected to a central control room or SCADA for remote operation, recipe management, and historical data tracking – perfect for quality control and traceability.
Technical Specifications (Typical Model)
| Parameter | Value / Range |
|---|---|
| Evaporation Capacity | 1,500 kg/h (adjustable) |
| Feed Concentration (Milk) | 8–12% solids |
| Final Concentration | Up to 45–50% solids (adjustable) |
| Operating Temperature | 60–85°C (under vacuum 0.2–0.5 bar) |
| Steam Pressure Requirement | 3–6 bar (g) |
| Power Supply | 380V / 50Hz (customizable) |
| PLC Brand | Siemens / Mitsubishi (or as requested) |
| Material – Product Contact | 304 SS (optional 316L) |
| Insulation & Cladding | Mineral wool + SS304 jacket |
Advantages for Your Dairy Business
- Preserve Product Quality: Low-temperature evaporation under vacuum prevents protein denaturation and maintains the natural flavor and nutritional value of milk.
- Reduce Operating Costs: PLC automation lowers labor costs and optimizes steam usage. Energy-saving options like MVR (Mechanical Vapor Recompression) can cut energy consumption by up to 50%.
- Enhanced Hygiene & Safety: 304 SS construction, CIP capability, and automatic alarms for temperature/pressure deviations ensure safe, hygienic operation.
- Flexible Production: Quick changeover between different milk types (whole, skim, whey) via programmable recipes – minimal downtime.
- Global Compatibility: Designed to meet international standards, with electrical components available for diverse voltage/frequency requirements.
At Qingdao Conqinphi Environmental Technology Group Co., Ltd., we have been dedicated to manufacturing high-quality evaporation equipment since 2015. Our factory employs 201–300 skilled workers and operates on a 10,000–30,000 m² area, with an annual export value of US$10 million to US$50 million. We have obtained multiple management system certifications including ISO9001, ISO14000, OHSAS18001 as well as industry-specific certifications like HACCP – demonstrating our commitment to quality, safety, and environmental responsibility.
Our products are exported to over 20 countries and regions, serving major dairy processors in Europe, North America, and Southeast Asia. We offer complete after-sales support, including installation guidance, commissioning, and spare parts supply. Every evaporator is factory-tested before shipment to ensure flawless performance.
Choose Conqinphi for your milk concentration needs – experience reliable technology, professional service, and a partnership that prioritizes your productivity. Contact our team today to discuss your specific requirements and receive a customized quotation!
Frequently Asked Questions (FAQ)
-
Q: What is the maximum concentration ratio achievable for whole milk?
A: The typical final total solids concentration can reach 45–50%, depending on the initial solids content and the specific configuration. Higher concentrations (e.g., up to 55%) are possible with a two-effect or multi-effect design – we can customize based on your target. -
Q: Can this evaporator handle liquids with high fouling tendency, like whey?
A: Yes. The long tube vertical design with PLC-controlled parameters minimizes hot spots and fouling. For high-fouling products, we recommend optional features like forced circulation or additional cleaning cycles. Our engineers can advise the best design for your specific product. -
Q: What utilities are required for operation?
A: The system typically requires steam (3–6 bar), cooling water, compressed air (for valves), and electricity. We provide a detailed utility consumption list with your proposal. -
Q: Is CIP (Clean-in-Place) system included?
A: The evaporator is designed for CIP compatibility. A dedicated CIP pump and tank can be supplied as optional components. The PLC can include CIP sequence programs. -
Q: What is the typical delivery time?
A: Standard lead time is 30–45 days after order confirmation, depending on capacity and customization. We can expedite for urgent projects. -
Q: Do you offer installation and commissioning services?
A: Yes, we provide on-site installation guidance and commissioning support by experienced engineers. Remote assistance is also available via video. -
Q: What certifications does your company hold?
A: We are certified under ISO9001, ISO14000, OHSAS18001, HACCP, and several other management systems. Our products can also be designed to meet FDA or GMP requirements upon request. -
Q: Can I visit your factory in Qingdao before placing an order?
A: Absolutely. We welcome factory inspections and trial runs. Please contact our sales team to schedule a visit.
For any further questions or to request a customized evaporator for your dairy plant, please reach out to our professional team. Qingdao Conqinphi Environmental Technology Group Co., Ltd. looks forward to being your reliable partner.

Send Inquiry to This Supplier


You May Also Like
-
PLC Controlled 500 Kg/h Sodium Chloride MVR Evaporation Crystallization System in 316L Stainless SteelUS$ 3220 - 7859000MOQ: 1 Combo
-
SS316L MVR Sodium Chloride Crystallization System – 50kW Compressor, 99.5% Purity Output, Skid MountedUS$ 3220 - 7859000MOQ: 1 Combo
-
Zero Liquid Discharge Solution – MVR Evaporation System for NaCl Recovery From Industrial WastewaterUS$ 3220 - 7859000MOQ: 1 Combo
-
MVR Evaporation Crystallization System for Salt Recovery – 2.5 T/h Evaporation Rate, Compact FootprintUS$ 3220 - 7859000MOQ: 1 Combo
-
All in One MVR Evaporation Unit for NaCl – 1000L/h Capacity, PLC Touchscreen, Low Energy Consumption DesignUS$ 3220 - 7859000MOQ: 1 Combo
-
MVR Sodium Chloride Crystallizer Used in Chemical Industry – Efficient Salt Separation and Brine ConcentrationUS$ 3220 - 7859000MOQ: 1 Combo
-
1 Year Warranty MVR NaCl Crystallization System With on Site Installation and Operator Training ServiceUS$ 3220 - 7859000MOQ: 1 Combo
-
Vacuum Evaporator for Pharmaceutical Wastewater Concentration, With 304 Shell and Tube Heat ExchangerUS$ 32600 - 8680000MOQ: 1 Combo
-
Vacuum Evaporator for Industrial Wastewater Treatment, Suitable for Electroplating and Metalworking EffluentUS$ 32600 - 8680000MOQ: 1 Combo
-
1 Year Warranty Vacuum Evaporator for Wastewater, Free Installation Guide and Technical SupportUS$ 32600 - 8680000MOQ: 1 Combo
