Contact Platform Support
 Help Center
Industrial Grade Double-Wall Safety Cabinet for Flammable Liquids -Corrosion Resistance for Manufacturing Facilities and Laboratories





Related Products
-
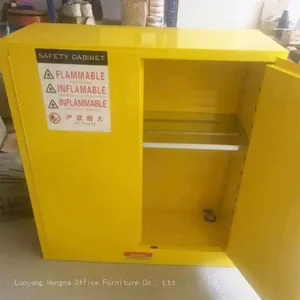
 Compact 12 Gallon Double-Wall Flammable Storage Cabinet- Laboratory Safety Cabinet for Chemical StorageUS$ 68 - 400MOQ: 2 Combos
-
45L Flammable Liquid Safety Cabinet- Premium Cold-Rolled Steel Construction (Yellow/Red/Blue)US$ 68 - 400MOQ: 2 Combos
-
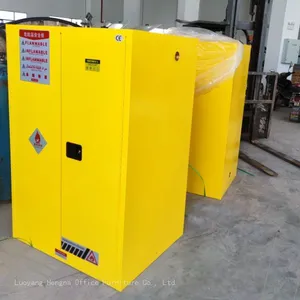
Yellow Flammable Storage Cabinet 45 Gallon for Lab & Workshop - Fireproof Chemical Safety Cabinet Steel IndustrialUS$ 60 - 700MOQ: 5 Combos
-
45 Gallon Flammable Safety Cabinet — OSHA CE Compliant, Compliance Costs Less Than a FireUS$ 60 - 700MOQ: 5 Combos
-
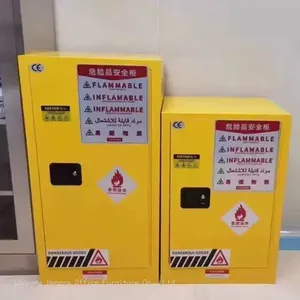
Colorful Fire-Resistant Chemical Cabinets for Laboratories & IndustriesUS$ 60 - 700MOQ: 5 Combos
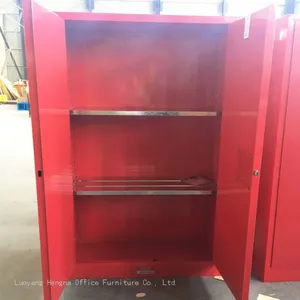
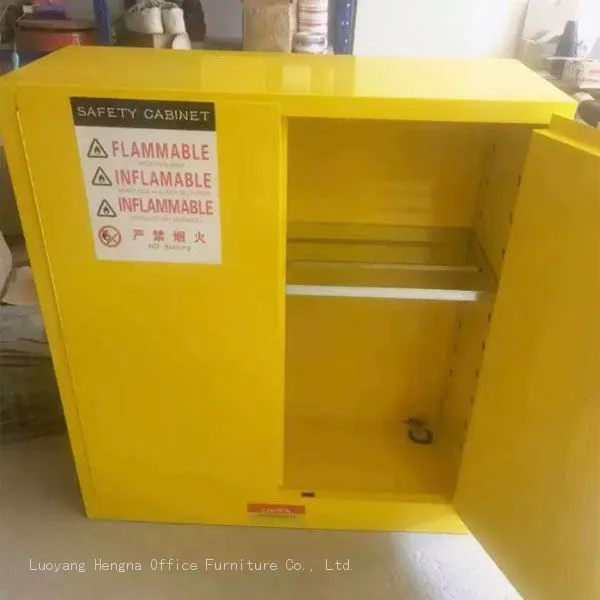
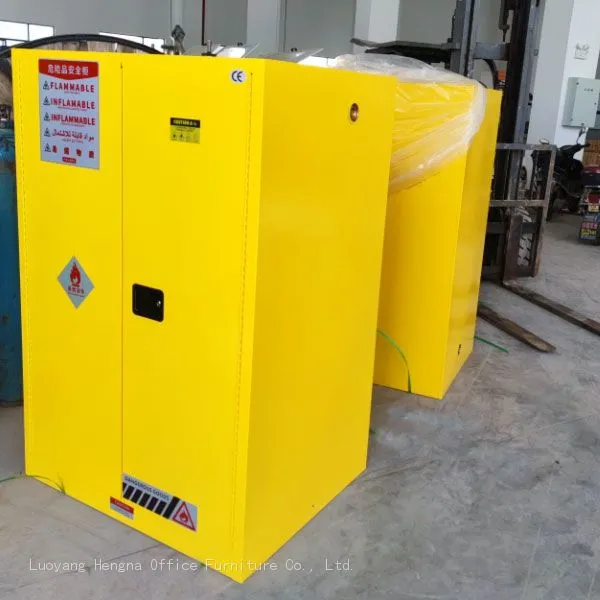
Industrial Grade Double-Wall Safety Cabinet for Flammable Liquids represents the ultimate in storage technology, combining heavy-duty steel construction with advanced corrosion resistance to provide unmatched protection for your valuable chemical inventory.
Designed specifically for high-traffic industrial environments and precision laboratory settings, these safety cabinets offer the perfect balance of robust construction, sophisticated safety features, and operational flexibility. The double-wall design provides critical fire protection, while the corrosion-resistant finish ensures longevity even in harsh chemical environments. As regulatory requirements continue to evolve, our industrial-grade cabinets remain at the forefront of safety technology, providing solutions that not only meet but exceed current standards.
Superior Construction and Materials
The foundation of our industrial-grade safety cabinet is its robust steel construction, engineered to withstand the rigors of demanding industrial environments:
Reinforced Steel Body: Constructed from 14-gauge cold-rolled steel for exceptional strength and durability, far exceeding industry standards.
Double-Wall Protection: Features dual steel walls with a 2-inch air gap between them, creating an effective thermal barrier that provides superior fire resistance compared to standard cabinets.
Welded Seams: All critical joints and seams are fully welded, eliminating potential weak points and ensuring maximum structural integrity under extreme conditions.
Reinforced Corners: Additional steel reinforcement at all corners and stress points prevents deformation and maintains cabinet integrity even when fully loaded.
The cabinet’s corrosion-resistant properties ensure long-term performance in harsh chemical environments:
| Corrosion Protection Feature | Description | Benefit |
|---|---|---|
| Epoxy Powder Coating | Multi-stage epoxy powder coating applied electrostatically | Provides superior chemical resistance and prevents rust formation |
| Galvanized Undercoating | Zinc galvanization applied before final coating | Creates additional barrier against corrosion and chemical damage |
| Chemical-Resistant Seals | Specialized seals on all doors and access points | Prevents chemical penetration and maintains cabinet integrity |
| Stainless Steel Hardware | All fasteners and hardware made from 316 stainless steel | Eliminates corrosion points and ensures long-term reliability |
Our industrial-grade safety cabinets incorporate multiple layers of fire protection:
Fire-Resistant Insulation: The air space between double walls is filled with specialized ceramic fiber insulation that can withstand temperatures up to 2000°F (1093°C) for extended periods.
Automatic Door Closing: Self-closing mechanisms with hydraulic dampers ensure doors close smoothly and securely every time, maintaining fire containment.
Intumescent Seals: Door seals feature intumescent material that expands when exposed to heat, creating an airtight barrier that prevents fire penetration.
Thermal Monitoring: Optional temperature monitoring systems provide real-time feedback on internal cabinet conditions, alerting personnel to potential issues.
Comprehensive static control systems prevent dangerous static discharge:
Integrated Grounding System: Heavy-duty grounding connectors with multiple attachment points ensure reliable static dissipation.
Conductive Interior Surfaces: All interior surfaces are treated with conductive coatings that work in harmony with the grounding system.
Static Dissipative Shelves: Adjustable shelves feature static dissipative properties that prevent static charge accumulation on stored containers.
Grounding Verification: Visual indicators confirm proper grounding connection, providing immediate verification of system integrity.
Our industrial-grade safety cabinets are available in multiple capacity options designed for demanding environments:
30-Gallon Model: Ideal for medium-sized industrial operations and larger laboratory settings.
45-Gallon Model: Perfect for facilities requiring substantial chemical storage capacity.
60-Gallon Model: Designed for industrial applications with extensive chemical inventory needs.
90-Gallon Model: Suitable for large-scale manufacturing operations and research facilities.
115-Gallon Model: The maximum capacity option for facilities with extensive chemical storage requirements.
We offer specialized configurations to meet specific industry requirements:
Laboratory Configuration: Features additional safety measures including vapor detection systems and enhanced ventilation for precision laboratory environments.
Manufacturing Configuration: Optimized for high-traffic industrial environments with reinforced construction and heavy-duty shelving systems.
Cleanroom Configuration: Designed for sterile environments with special finishes and filtration systems that maintain cleanroom integrity.
Outdoor Configuration: Enhanced weatherproofing and additional corrosion protection for outdoor installations in harsh environments.
In manufacturing environments, our industrial-grade cabinets provide critical protection for flammable liquids used in production processes. The heavy-duty construction withstands the demands of high-traffic areas, while the corrosion resistance ensures longevity even when exposed to various chemicals and cleaning agents.
Research LaboratoriesLaboratory settings require precision and safety, which our cabinets deliver through specialized configurations that accommodate the unique needs of research environments. The enhanced ventilation systems and static control features are particularly valuable in settings where sensitive experiments are conducted.
Pharmaceutical ProductionPharmaceutical facilities demand the highest levels of purity and safety. Our cabinets provide secure storage that prevents contamination while ensuring compliance with strict regulatory requirements specific to the pharmaceutical industry.
Chemical Processing PlantsIn chemical processing environments, where exposure to corrosive substances is constant, our advanced corrosion protection features ensure long-term performance and reliability. The heavy-duty construction provides the durability needed for these demanding applications.
Technical Specifications and Performance DataConstruction Specifications| Component | Specification | Performance Benefit |
|---|---|---|
| Body Material | 14-gauge double-walled steel | Superior structural integrity and fire resistance |
| Insulation | 2-inch ceramic fiber insulation | Exceptional fire protection up to 2000°F |
| Door Construction | 14-gauge steel with reinforced edges | Enhanced durability and security |
| Shelf Capacity | Up to 600 pounds per shelf | Accommodation of heavy containers |
| Finish | Multi-stage epoxy powder coating | Superior corrosion and chemical resistance |
Q: What makes this cabinet “industrial grade” compared to standard safety cabinets?
A: Our industrial-grade cabinets feature heavier construction (14-gauge vs. 18-gauge steel), enhanced corrosion protection, reinforced structural components, and more robust safety systems. These features make them suitable for demanding industrial environments where standard cabinets might fail.
Q: How does the double-wall construction enhance fire protection?
A: The double-wall construction creates an air gap between walls that acts as a thermal barrier, significantly slowing heat transfer during fire events. This design provides critical time for emergency response and prevents cabinet contents from reaching ignition temperatures.
Q: Can these cabinets be customized for specific industry requirements?
A: Yes, we offer extensive customization options including specialized finishes, enhanced ventilation systems, advanced monitoring capabilities, and industry-specific configurations to meet unique operational requirements.
Q: What maintenance is required for these industrial-grade cabinets?
A: Regular maintenance includes monthly inspections of door operation and safety systems, quarterly testing of grounding and static control systems, and annual professional inspections to assess overall condition and compliance.
Q: Are these cabinets suitable for cleanroom environments?
A: Yes, we offer specialized cleanroom configurations with appropriate finishes, filtration systems, and construction materials that maintain cleanroom integrity while providing required safety features.

Send Inquiry to This Supplier


You May Also Like
-
High-class Chemical Safety Cabinets for Flammable Liquids: OSHA Compliant Storage SolutionsUS$ 60 - 700MOQ: 5 Combos
-
Secure Chemical Storage Cabinets: Flame-Resistant and DurableUS$ 60 - 700MOQ: 5 Combos
-
Explosion-Proof Storage for Chemicals: Fire Safety CabinetsUS$ 60 - 700MOQ: 5 Combos
-
Durable Fireproof Storage Cabinets for Hazardous MaterialsUS$ 60 - 700MOQ: 5 Combos
-
Flammable Liquid Storage Solutions for Chemical & Industrial SafetyUS$ 60 - 700MOQ: 5 Combos
-
High- Capacity Secure Hazardous Material Gallon Cabinet With Three-point Locking System for Laboratories and Industrial UseUS$ 60 - 700MOQ: 5 Combos
-
Muti-Color Explosion-Proof Chemical Storage for Gallon Containers – Safe for Toxic Materials and Ideal for Storing Flammable LiquidsUS$ 60 - 700MOQ: 5 Combos
-
Industrial Chemical Safety Steel Gallon Cabinet With Ventilation Ports for Flammable & Corrosive Liquids – 45 GallonUS$ 60 - 700MOQ: 5 Combos
-
Fire-Proof Colorful Chemical Storage Cabinet With Safe Lock for Laboratories – Safe Storage for Gallon ChemicalsUS$ 60 - 700MOQ: 5 Combos
-
Fire-Resistant Chemical Cabinet for Gallon-Sized Containers in Industrial Settings- Compliant With Safety RegulationsUS$ 60 - 700MOQ: 5 Combos