


 Contact Platform Support
 Help Center
Ion Exchange Membrane Chlor Alkali Process Plant







Related Products
-
 Automated Chlor Alkali Manufacturing UnitUS$ 100000 - 2000000MOQ: 1 Set
-
Industrial 31% Hydrochloric Acid SolutionUS$ 100000 - 2000000MOQ: 1 Set
-
High Purity Liquid Chlorine via Chlor-Alkali Process for Chemical SynthesisUS$ 100000 - 2000000MOQ: 1 Set
-
Purified Industrial Chlorine Gas for Water Treatment DisinfectionUS$ 100000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Process Caustic Soda for Chemical & Water TreatmentUS$ 200000 - 2000000MOQ: 1 Set
1 Product Overview
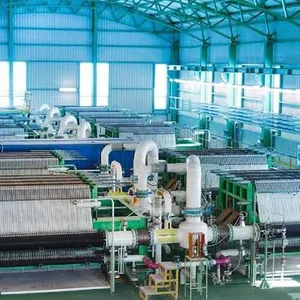
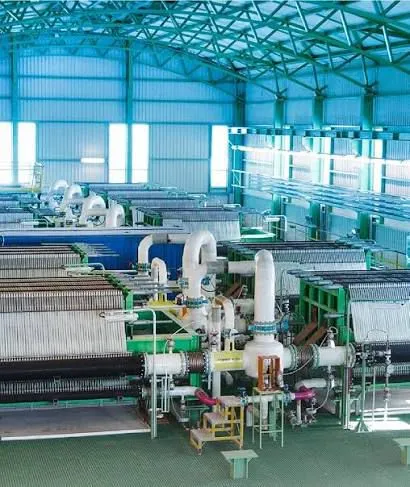
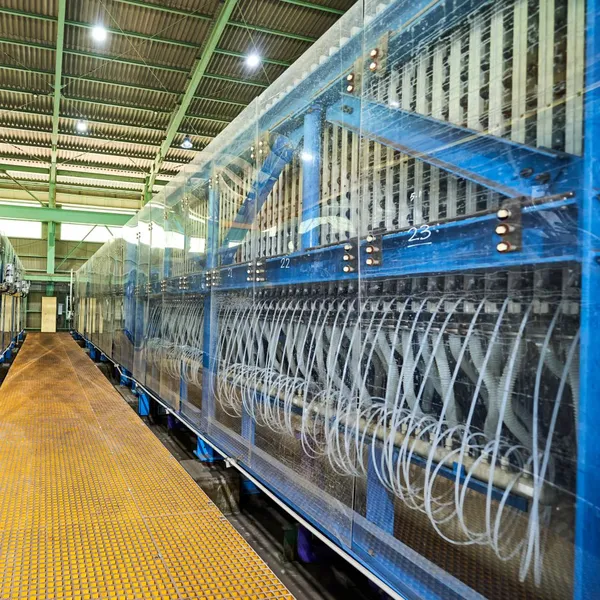
The chlor alkali process plant is a core industrial electrolysis system designed for mass production of basic chemical raw materials through saturated brine electrolysis. As a modern green chemical production solution, it adopts advanced ion exchange membrane technology to replace traditional high-pollution chlor alkali processes. The system uses industrial refined brine as the sole raw material to continuously produce sodium hydroxide (caustic soda), chlorine gas and hydrogen gas, three essential raw materials widely used in the global chemical industry.
Different from conventional chlor alkali equipment, this production line realizes closed-loop brine recycling, fully automatic operation and zero mercury emission. It effectively solves the pain points of traditional equipment such as high energy consumption, serious pollution, unstable product purity and complicated maintenance. Suitable for large-scale chemical factories, industrial parks and supporting chemical production projects, this chlor alkali system provides stable, compliant and cost-effective bulk chemical manufacturing capacity for modern industrial production.
2 Technical Principle
The chlor alkali production system operates based on selective ion exchange membrane electrolysis technology. After multi-stage precision purification, softening and filtration, saturated industrial brine is injected into the anode chamber of the electrolytic cell, while deionized water is added to the cathode chamber. Under stable DC power supply, directional electrochemical reactions take place inside the sealed electrolytic unit.
At the anode, chloride ions lose electrons and oxidize into chlorine gas. Sodium ions pass through the high-selectivity cation membrane and migrate to the cathode side. At the cathode, water molecules are reduced to generate hydrogen gas and hydroxide ions, which combine with sodium ions to form high-purity sodium hydroxide solution. The ion membrane completely isolates anode and cathode substances to avoid cross-contamination and side reactions. All generated gas products are collected through sealed pipelines, and the residual brine is recycled and reused after treatment, forming a complete green industrial electrolysis cycle.
3 Main Features
Green and Pollution-Free Production: The entire process completely abandons mercury-based electrolysis, achieving zero heavy metal discharge and low wastewater emission. The closed circulating brine system greatly reduces raw material waste and meets global industrial environmental protection and carbon neutrality requirements.
Stable High-Purity Output: Precision membrane separation and constant current electrolysis ensure consistent product purity. The produced caustic soda features low impurity content, while chlorine and hydrogen maintain stable concentration, fully compliant with industrial chemical raw material standards.
Low Energy Consumption & High Efficiency: Optimized zero-gap electrolytic cell structure and intelligent rectifier power supply lower electrolysis voltage and reduce unit power consumption. The overall brine conversion rate is significantly improved compared with traditional process equipment.
Fully Automated Intelligent Operation: Equipped with industrial PLC automatic control system, the equipment realizes automatic brine feeding, online parameter adjustment, intelligent temperature and pressure control, automatic gas collection and liquid discharge. It supports long-term unattended continuous operation.
Intrinsic Safety Design: Adopting fully sealed gas-liquid separation structure and independent gas conveying pipelines, the system effectively prevents chlorine and hydrogen mixing. It is equipped with overpressure, overheating and leakage protection to eliminate explosion and poisoning risks.
Flexible Capacity Expansion: Modular unit design allows single-unit independent operation and multi-unit parallel expansion. Production load can be adjusted steplessly to adapt to small-batch trial production and large-scale continuous industrial production.
4 Core Advantages
Advanced Process Upgrade: Adopting the most mainstream ion membrane process in the global chlor alkali industry, it eliminates the technical defects of diaphragm and mercury electrolysis. The equipment runs stably with long service life and low failure rate, suitable for long-cycle industrial production.
Excellent Economic Benefits: High raw salt utilization rate reduces material cost; intelligent energy-saving control cuts power consumption; zero pollution treatment cost reduces environmental protection investment. Recyclable by-products further improve overall project revenue.
Reliable Product Quality Control: The system precisely controls electrolysis current density, liquid temperature, brine concentration and operating pressure. All finished chemical products maintain stable quality, fully meeting the raw material requirements of downstream fine chemicals, environmental protection and pharmaceutical industries.
Strict Safety Guarantee: Multiple interlock protection mechanisms including emergency shutdown, gas concentration monitoring, pressure relief protection and water level interlock ensure intrinsically safe production. It avoids toxic gas leakage and equipment failure risks.
Strong Project Adaptability: The whole production line can be customized according to customer output demand, site space and brine quality conditions. It supports new project construction and old chlor alkali production line renovation and upgrading.
5 Core Components
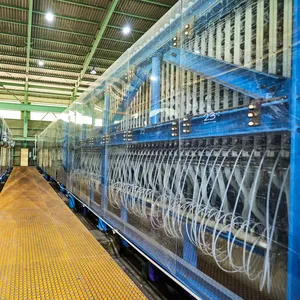
Ion Exchange Membrane Electrolyzer: The core reaction component of the chlor alkali system. It adopts corrosion-resistant titanium-based electrode and high-stability cation exchange membrane, featuring high electrolysis efficiency, strong anti-pollution ability and long service life.
Intelligent DC Rectifier System: Converts industrial AC into stable adjustable DC power for electrolysis. It ensures constant current and voltage output, adapts to grid fluctuation and guarantees consistent electrolysis efficiency.
Multi-Stage Brine Purification System: Including raw salt dissolving unit, precision filter, hardness removal and impurity removal device. It removes calcium, magnesium, suspended solids and organic impurities to ensure qualified brine inlet quality and protect the electrolytic membrane.
PLC Industrial Automatic Control Cabinet: Realizes full-process intelligent management including feeding, electrolysis, temperature control, pressure stabilization, gas collection and liquid discharge. It supports real-time data monitoring, fault alarm and remote operation.
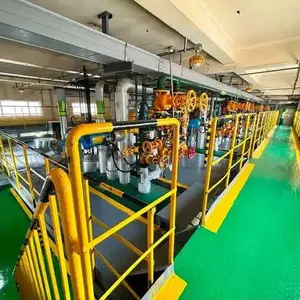
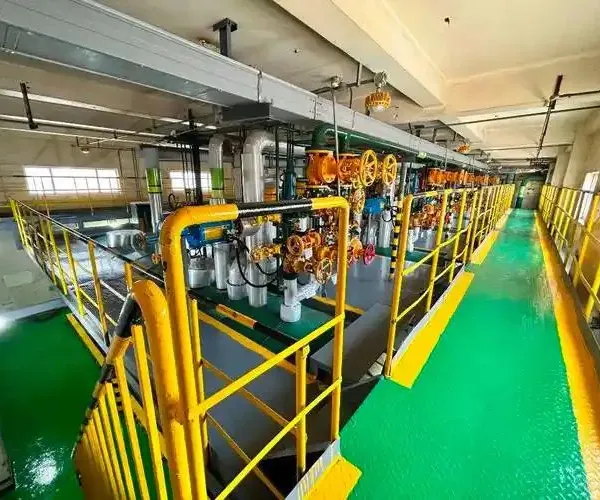
Closed Gas-Liquid Separation & Recovery Unit: Separates and collects chlorine, hydrogen and lye independently. It prevents gas cross-mixing, ensures safe gas recycling and avoids environmental pollution caused by exhaust emission.
Circulating Cooling and Pressure Stabilizing System: Controls the operating temperature and internal pressure of the electrolytic cell in real time, prevents equipment overheating and overpressure damage, and ensures long-term stable operation of the production line.
6 Application Fields
Basic Chemical Industry: Provides industrial-grade caustic soda, chlorine and hydrogen for the production of inorganic chemicals, alkali products, salt chemicals and basic chemical raw materials.
Fine Chemical & Pharmaceutical Industry: Supplies high-purity chemical raw materials for pesticide synthesis, pharmaceutical intermediates, dye production, chemical additives and surfactant manufacturing.
Environmental Protection & Water Treatment Industry: Supporting flue gas desulfurization, wastewater pH adjustment and industrial water disinfection raw material preparation for environmental protection projects.
Paper & Textile Industry: Provides high-quality caustic soda for pulping and papermaking, textile printing and dyeing, fiber modification and industrial washing processes.
Metallurgy & Electroplating Industry: Used for metal smelting auxiliary treatment, electroplating cleaning solution preparation and industrial metal surface alkali treatment.
New Energy & Advanced Materials: Supplies high-purity hydrogen energy raw materials and battery-grade caustic soda for new energy materials, hydrogen energy utilization and advanced chemical material production.
Boasting 25 years of professional industry experience in production and supply, ZLN factory delivers premium,cost-effective chemical products with reliable quality. Equipped with fully automatic production systems and scientific modular production line design, we achieve stable output, high efficiency and low energy consumption while strictly complying with industrial standards. Different from ordinary manufacturers, ZLN provides flexible customized services tailored to diverse customer needs on product specifications, packaging and solutions. With direct factory pricing and optimized production processes, we help clients cut procurement costs and obtain high-quality, stable chemical supplies with comprehensive professional support.

Send Inquiry to This Supplier


You May Also Like
-
Chlor-Alkali Process Liquid Chlorine for Disinfection & SynthesisUS$ 200000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Process Hydrochloric Acid for Metal Pickling & Chemical ProcessingUS$ 200000 - 2000000MOQ: 1 Set
-
Chlor-Alkali Plant EPC Project | Turnkey Solution for Caustic Soda & Hydrochloric Acid ProductionUS$ 100000 - 2000000MOQ: 1 Set
-
99% Caustic Soda Flakes EPC Project | Turnkey Industrial Solid NaOH Production PlantUS$ 100000 - 2000000MOQ: 1 Set
-
33% Hydrochloric Acid Equipment | Corrosion Resistant Industrial HCl Production Plant SystemUS$ 100000 - 2000000MOQ: 1 Set
-
Liquid Chlorine Equipment | Industrial Liquid Chlorine Production, Storage & Handling SystemUS$ 100000 - 2000000MOQ: 1 Set
-
Ion Membrane Chlor-Alkali Plant EPC Turnkey ProjectUS$ 100000 - 2000000MOQ: 1 Set
-
99% High Purity Caustic Soda Flakes EPC Turnkey LineUS$ 100000 - 2000000MOQ: 1 Set
-
31% Industrial Grade Hydrochloric Acid Synthesis EquipmentUS$ 100000 - 2000000MOQ: 1 Set
-
Industrial Liquid Chlorine Complete EquipmentUS$ 100000 - 2000000MOQ: 1 Set


