


 Contact Platform Support
 Help Center
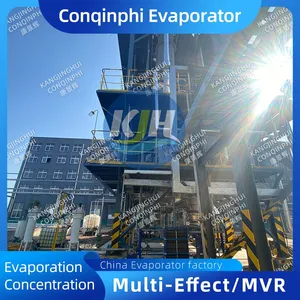
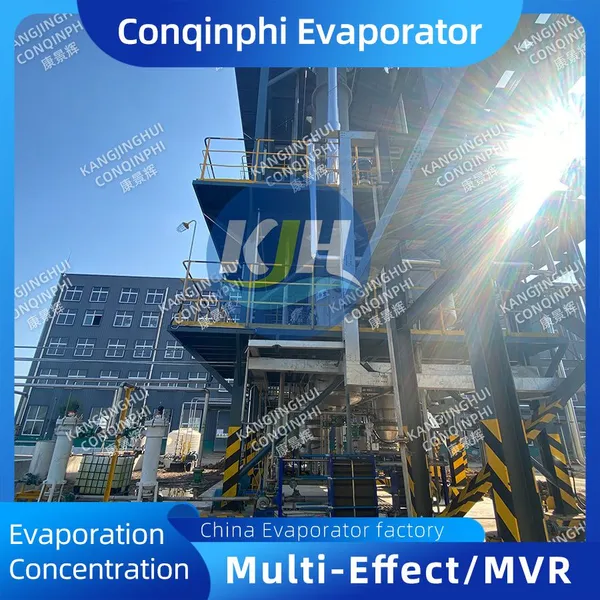
Used in Pharmaceutical Industry: Flame Retardant Triple-Effect Evaporator, Solvent Recovery






Product Spotlights




Related Products
-
 220V Automatic Flame Retardant Triple-Effect Evaporator, 500L/H Capacity, Standard CompliantUS$ 52380 - 8639000MOQ: 1 Combo
-
304 Stainless Steel Flame Retardant Triple-Effect Evaporator With PLC Control for Chemical ProcessingUS$ 52380 - 8639000MOQ: 1 Combo
-
Steam-Heated Flame Retardant Triple-Effect Evaporator, 316L Stainless Steel, Vacuum OperationUS$ 52380 - 8639000MOQ: 1 Combo
-
Energy-Saving Flame Retardant Triple-Effect Evaporator, PLC Touch Screen, 10kW PowerUS$ 52380 - 8639000MOQ: 1 Combo
-
Compact Large Triple-Effect Evaporator, PLC Control, 304 SS, 220V, 50HzUS$ 7380 - 574000MOQ: 1 Combo
Welcome to Qingdao Conqinphi Environmental Technology Group Co., Ltd. – your trusted partner in advanced environmental solutions. As a specialized manufacturer established in 2015, we are proud to present our Flame Retardant Triple-Effect Evaporator, specifically designed for solvent recovery in the pharmaceutical industry. This equipment combines high-efficiency triple-effect evaporation with built-in flame retardant safety features, ensuring maximum solvent recovery rates while minimizing fire hazards. With our factory spanning 10,000-30,000 square meters and a dedicated team of 201-300 employees, we deliver robust, reliable, and customizable systems that meet the rigorous demands of pharmaceutical production.
Key Features & Technical Specifications
- Triple-Effect Evaporation Design: Utilizes three stages of heat recovery to achieve up to 30% energy savings compared to single-effect systems. Each effect operates at a lower temperature, preserving solvent quality and reducing thermal degradation.
- Flame Retardant Construction: All electrical components, insulation materials, and structural elements are manufactured with flame-retardant materials. The system is equipped with explosion-proof motors, spark-proof switches, and automatic fire suppression interfaces, making it suitable for handling volatile organic solvents.
- High Solvent Recovery Rate: Capable of recovering over 95% of solvents from pharmaceutical waste streams, such as ethanol, methanol, acetone, and ethyl acetate. The system ensures minimal loss and high purity of recovered solvents.
- PLC Automatic Control: Optional programmable logic controller (PLC) with touch-screen interface allows real-time monitoring of temperature, pressure, flow rate, and liquid level. Data logging and remote alarm functions are available for seamless integration into existing plant automation.
- Customizable Capacity: From 500 L/h to 10,000 L/h evaporation capacity, tailored to your specific production scale. The unit can be designed for continuous or batch operation.
- Material Options: Standard construction in 304L or 316L stainless steel, with optional Hastelloy for corrosive solvents. All wetted parts are polished to a surface finish of Ra ≤ 0.8 μm, meeting pharmaceutical hygiene standards.
- Compact Footprint & Skid-Mounted Design: Pre-assembled on a heavy-duty skid, reducing installation time and space requirements. The unit can be easily relocated if needed.
Technical Parameters (Example Model)
| Parameter | Value |
|---|---|
| Evaporation Capacity | 2,000 L/h (water evaporation) |
| Number of Effects | 3 |
| Operating Temperature | 60°C - 120°C (adjustable per effect) |
| Steam Consumption | Approx. 0.4 kg steam per kg solvent evaporated |
| Power Consumption | 15 kW (pumps, controls, auxiliary) |
| Solvent Recovery Rate | ≥95% for typical solvents |
| Purity of Recovered Solvent | ≥99% (depending on feed composition) |
| Noise Level |
Benefits for Your Pharmaceutical Production
- Enhanced Safety: The flame retardant design significantly reduces the risk of fire or explosion during solvent recovery, protecting your personnel and facility. This is critical when handling flammable solvents like ethanol or acetone.
- Cost Savings: By recovering high-purity solvents, you reduce the need to purchase fresh solvents, lowering raw material costs. The triple-effect energy efficiency also cuts steam consumption, reducing operational expenses.
- Environmental Compliance: Minimize waste discharge and volatile organic compound (VOC) emissions. The system helps you meet stringent environmental regulations, such as those from EPA or local authorities.
- Product Quality: Gentle evaporation at lower temperatures prevents solvent degradation, ensuring that recovered solvents maintain their original properties for reuse in pharmaceutical processes.
- Easy Maintenance: Modular design with accessible components simplifies cleaning and inspection. CIP (clean-in-place) nozzles are optional for automated cleaning between batches.
Why Choose Qingdao Conqinphi?
With over 9 years of experience since 2015, we have established a strong reputation in the global environmental technology market. Our factory covers 10,000-30,000 square meters, equipped with advanced manufacturing and testing facilities. We hold multiple certifications including ISO9001, ISO14000, OHSAS18001, HACCP, SA8000, and others, demonstrating our commitment to quality, environmental management, and social responsibility. Our annual export value exceeds US$10 million, with products shipped to North America, South America, Europe, Southeast Asia, Africa, and more. We serve clients in the pharmaceutical, chemical, food, and wastewater industries. Our team of 201-300 skilled professionals ensures that every evaporator is designed, fabricated, and tested to meet your exact specifications. We offer comprehensive after-sales support, including installation guidance, commissioning, and remote troubleshooting. Contact us today to discuss your solvent recovery needs and receive a customized solution that maximizes efficiency and safety.
Frequently Asked Questions
-
Q: What solvents can this evaporator handle?
A: The system is designed for common pharmaceutical solvents such as ethanol, methanol, isopropanol, acetone, ethyl acetate, and toluene. For corrosive or high-boiling-point solvents, we can customize materials and operating parameters. -
Q: Is the flame retardant feature certified?
A: Our design complies with international safety standards for explosion-proof environments. We can provide documentation upon request, though specific certifications depend on your local regulations. We recommend consulting with our engineering team for compatibility. -
Q: What is the typical lead time?
A: For standard models, lead time is approximately 8-12 weeks after order confirmation. Customized units may require 12-16 weeks, depending on complexity. -
Q: Can the system be integrated with existing solvent recovery lines?
A: Yes, our evaporator can be supplied with inlet/outlet flanges meeting your piping specifications. The PLC control system can also interface with your plant DCS via Modbus or Profibus, if required. -
Q: How do you ensure the purity of recovered solvents?
A: The triple-effect design includes a demister and optional rectification column to separate low-boiling impurities. Final purity depends on feed composition; we can design for purity levels up to 99.9% if needed. -
Q: What after-sales support do you provide?
A: We offer 12-month warranty on materials and workmanship. Technical support is available via email, phone, or video call. Spare parts are available for quick delivery from our Qingdao warehouse. -
Q: Is training provided for operators?
A: Yes, we provide on-site or remote training for your staff, covering operation, maintenance, and safety procedures. Detailed manuals are included. -
Q: Do you have references from pharmaceutical companies?
A: We have supplied similar systems to multiple pharmaceutical manufacturers in China and abroad. References can be provided upon request after signing a non-disclosure agreement.

Send Inquiry to This Supplier


You May Also Like
-
Industrial Large Triple-Effect Evaporator, 304 Stainless Steel, 380V, 2000L/HUS$ 7380 - 574000MOQ: 1 Combo
-
Large Triple-Effect Evaporator With Technical Training and Spare Parts, PLC Control, 304 SSUS$ 7380 - 574000MOQ: 1 Combo
-
Automatic Large Triple-Effect Evaporator, 304 SS, 220V, 2000L/H CapacityUS$ 7380 - 574000MOQ: 1 Combo
-
Large Triple-Effect Evaporator for Wastewater Treatment, Energy Saving, 304 SSUS$ 7380 - 574000MOQ: 1 Combo
-
304 Stainless Steel Large Triple-Effect Evaporator With PLC Control and 380V PowerUS$ 7380 - 574000MOQ: 1 Combo
-
Large Triple-Effect Evaporator With CIP Cleaning System, 304 SS, Automatic OperationUS$ 7380 - 574000MOQ: 1 Combo
-
Large Triple-Effect Evaporator for Pharmaceutical Production, 304 Stainless Steel, CIPUS$ 7380 - 574000MOQ: 1 Combo
-
Large Triple-Effect Evaporator With 1-Year Warranty and Mill Test Report, 304 SSUS$ 7380 - 574000MOQ: 1 Combo
-
Energy-Saving Large Triple-Effect Evaporator, PLC Touch Screen, 304 Stainless Steel, 380VUS$ 7380 - 574000MOQ: 1 Combo
-
Triple-effect Evaporator Equipment With PLC Control Evaporation Capacity 300-3000L/h 220V/380VUS$ 3250 - 882000MOQ: 1 Combo
